Resources
Industry insights, product updates & customer wins
Stay up to date with industry insights, customer stories, and product improvements—everything to help you quote faster and run smoother.
Success stories
0
min read
From quoting crunches to streamlined processes: Tempus Tools empowers growth of J&T Steel Sales
As J&T Steel Sales expanded into the fast-growing laser cutting market, outdated spreadsheet-based quoting quickly became a bottleneck for delivering fast, reliable service. By adopting Tempus Tools, the team streamlined quoting, order tracking, and invoicing—freeing up time, improving consistency, and supporting the company’s growth as they scale their laser cutting operations.
Expanding Australian metal fabrication specialist, J&T Steel Sales, has found that improved productivity and new equipment is only half the battle to boost customer service and sales – equally important is eliminating the outdated processes used to track and prepare quotes, delivery, and invoices.
J&T Steel Sales began as a small plate processing business in Victoria with a CNC Plasma machine, where staff used spreadsheets to develop quotes for customers, but the company has now made the move into the high demand laser cutting market.
Part of the motivation for the expansion was a need in the market for better lead times on laser cut metal products, including aluminium, stainless steel, and carbon steel.
“We had customers come and beg us to purchase a laser machine, because they were fed up with the long lead times that were becoming increasingly common for laser cut products,” explains Luke Patterson, Operations Manager, J&T Steel Sales.
“So we invested in a laser cutting machine, and prepared to grow our business to the next level. But with this change, we needed a quick and efficient software solution to export a presentable quote that we can forward directly to customers in a timely fashion. Spreadsheets just weren’t going to work anymore, so we did some research and found Tempus Tools,” he said.
Laser cutting quoting software streamlines operationsTempus Tools, is a multi-functional laser cutting quoting software that is provided using a SaaS (Software as a Service) model. Tempus Tools was developed specifically for the laser cutting industry, and is designed to save job shops time, and make quoting more efficient, accurate, and consistent.
“Tempus Tools has allowed us to streamline not only the quoting aspect, but also the tracking of active orders as well as invoicing,” says Luke.
“It has been able to take most of the heavy lifting in cutting back on excess paper waste in our offices, whilst also creating a digital paper trail to be able to track material usage and stock.”
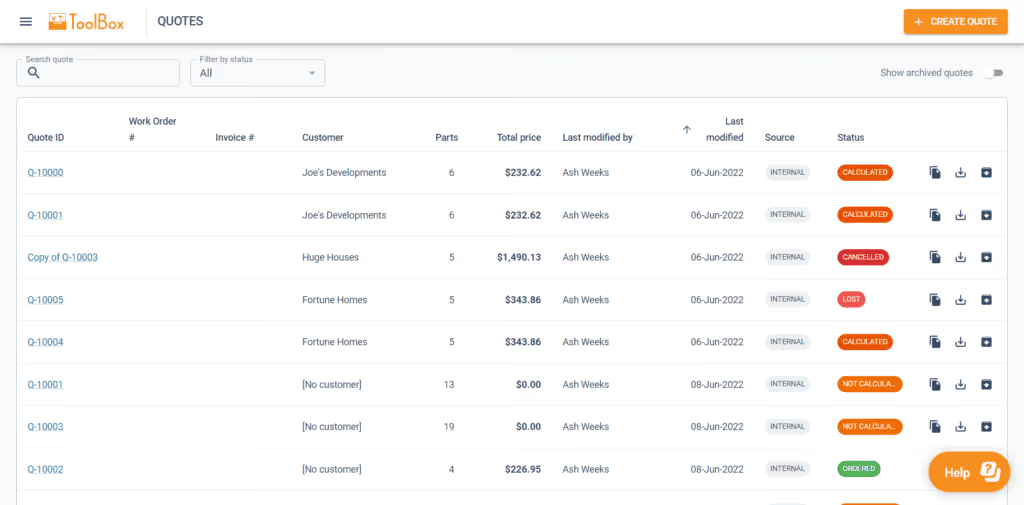
Since purchasing the laser cutting machine, J&T Steel Sales has committed to getting customers their parts when they need them, calling it “the J&T Guarantee”.
“Tempus Tools has helped us immensely in delivering this guarantee to our customers. It has taken the stresses and late night quoting crunches and completely streamlined the process, freeing up more time for us to be able to focus on growing the business,” says Luke.
“In the past, expanding our customer base meant we would fall increasingly behind when it came to invoicing and quoting. Now, with Tempus Tools, we really feel we have found a software that not only services us now, but also allows us room to grow in the future.”
Service is key
Luke explains that in his business, customer service is the key to success. Customers have good memories, and they value pricing consistency, accuracy, and reliability.
“Being a service-focused business, it’s something I look for in our suppliers too. In my opinion, the Tempus Tools team has been exceptional when it comes to responsiveness and availability to work through any challenges I’m experiencing,” he says.
“Coming from a small business ourselves it was an incredibly refreshing experience to have team members visit our workshop, and to also feel listened to when it came to our concerns or feedback for the future development of Tempus Tools.”
“I met Mark Washington (Sales & Support) and Felipe Lechuga (Director) from Tempus Tools at a local manufacturing expo earlier this year, and they took the time to visit our job shop and discuss the functionality of Tempus Tools, and what more it could be doing for us. I was very impressed, and I’m grateful for all the support.”
A bright future
J&T Steel Sales has seen steady growth since moving into the laser cutting business, and Luke has plans to continue this trend.
“Our future plans are not only to focus on bringing in new customers – ideally ones that require repeat work – but also to let all our customers know about our bending and fabrication facility, so they know we can provide an end-to-end manufacturing solution,” he says.
“Tempus Tools has a huge range of useful features, and the development team is always working on new functionality that can benefit job shops like ours, so it is a key component of our growth plans.”
To learn more about Tempus Tools, please click here.
Read blog
Product updates
0
min read
Tempus Tools’ Google Drive integration: 6 ways to supercharge your job shop efficiency
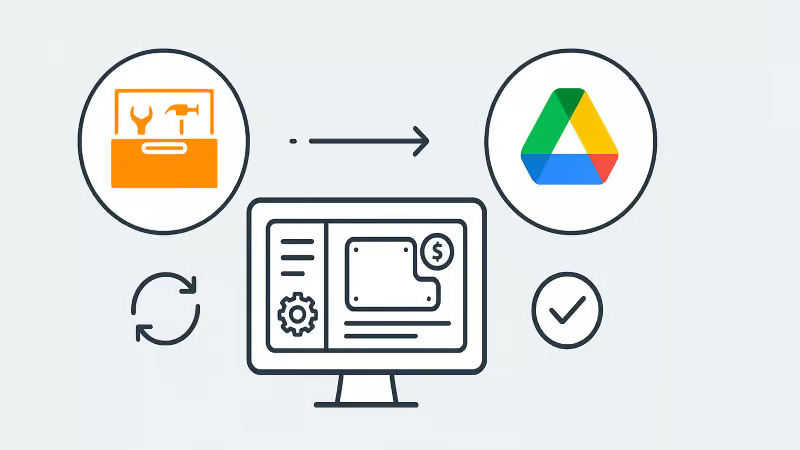
Last month Tempus Tools released a powerful new feature: seamless integration with Google Drive.
Since then, we’ve heard from lots of customers about the innovative ways they have implemented this integration in their job shops, and we wanted to share the best six with you to inspire you to use the feature in your shop.
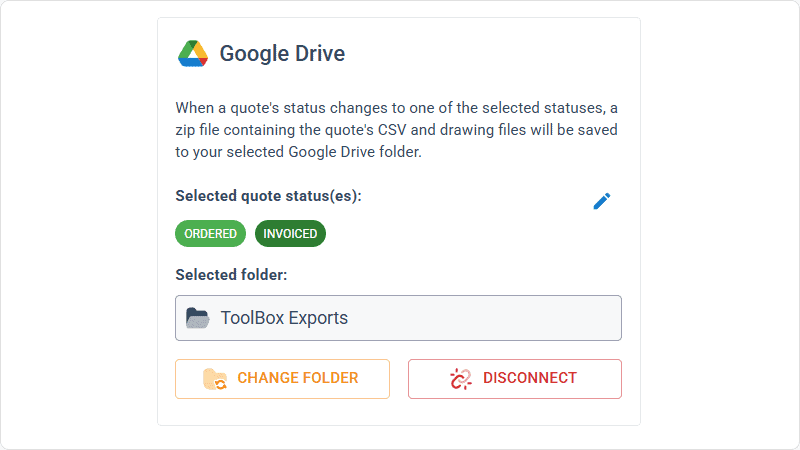
First, a quick recap: with the Google Drive integration, all your quote data (in CSV format) and production-ready part files can be automatically saved to your chosen Google Drive folder. From here, they can be exported to any number of programs or that data can be manipulated for many use cases, opening up a world of automation, reporting and connectivity for your job shop. We’ve also put together a quick video to show the integration in action.
1. Automate quote data collection for reporting
With every quote automatically saved, you can easily compile and analyse your quote performance over time. Use Google Sheets or your favourite analytics tool to track:
- win/loss rates
- performance across material types
- average order size
- breakdown of secondary processes contributions
This data-driven approach helps you identify trends, optimise pricing and improve customer response times.
2. Connect with ERP/MRP and other business systems
Some apps have native integration with Google Drive, which makes taking in quote data and parts easy, but many need a formal API. Luckily, Google Drive comes with its own API.
Some users have used the Google Drive API to build automations that push quote data directly into ERP, MRP or order management systems. This can streamline order processing, reduce manual data entry and ensure your production schedule is always up to date.
3. Organise your orders by material type
Use the exported quote data to create a parts planner that groups jobs by common material type. This enables you to:
- batch similar jobs for more efficient material usage
- reduce changeover times on machines
- optimise purchasing and inventory management
A simple Google Sheets script or integration with a dashboard tool can make this process nearly automatic.
4. Integrate with project management tools
Connect your quote data with popular tools like ClickUp, Monday.com or Airtable. Build custom dashboards and planners for your factory, visualise job statuses and assign tasks to your team-all based on real-time quoting data. These tools don’t require coding or a developer and anyone can work wonders. These types of projects boost collaboration on the shop floor and keep everyone aligned on priorities.
5. Create a scheduling calendar from time calculations
Use the time estimates in your quote data to automatically populate a production calendar. With a Google Calendar integration, you can:
- visualise machine and operator workloads
- identify bottlenecks before they happen
- easily adjust schedules as new jobs come in
This proactive scheduling helps you deliver on time, every time.
6. Enable automated notifications and workflows
Set up Google Drive triggers (using tools like Zapier or Google Apps Script) to notify your team when new quotes are confirmed as orders, or to kick off downstream processes-like updating CRM records or ordering materials.
Getting started is easy
- Go to Settings > Organisation settings > Integrations in your Tempus Tools Tempus Tools account
- Connect your Google Drive and select your preferred folder
- Choose the quote statuses that will trigger automatic file saving
- Start building automations and workflows that fit your shop’s needs
This integration is designed to be flexible-whether you want to automate reporting, connect with business systems, or simply keep your files organised, Tempus Tools and Google Drive make it possible.
Ready to enhance your job shop efficiency? Try the new Google Drive integration today.
Read blog
Articles
0
min read
Is expensive, non-dedicated software holding you back from effortless laser cutting quoting?
Laser cutting is a precise task, requiring machinery tailored to specific requirements. Profitability is significantly boosted by the ability to be able to respond quickly to customer requests for quotes (RFQs), and efficiently deliver the product.
“With the time and energy often spent on selecting the right laser cutting machine, it’s amazing how often software is overlooked as a driver of productivity,” says Tempus Tools Head of Global Sales, Mark Washington.
“Sometimes laser cutting companies are stuck using software that wasn’t specifically designed for job shops, but it’s all that their team is used to using. Other times, expensive software is implemented, but only a small fraction of the features are actually used,” he says.
“And in many cases, it becomes so complex that a specialist is hired to manage quoting via the software – but what happens if they leave the company?”
Tempus Tools is the creator of dedicated quoting software, Tempus Tools, which can provide fast, accurate, and consistent laser cutting quotes that are professionally presented, ready to send back to the customer.
“Using software that isn’t specifically designed for laser cutting is like using a cricket bat to play tennis. It might get the job done, but it would be far more efficient and accurate with the tools designed for the job!” says Mark (pictured, right).
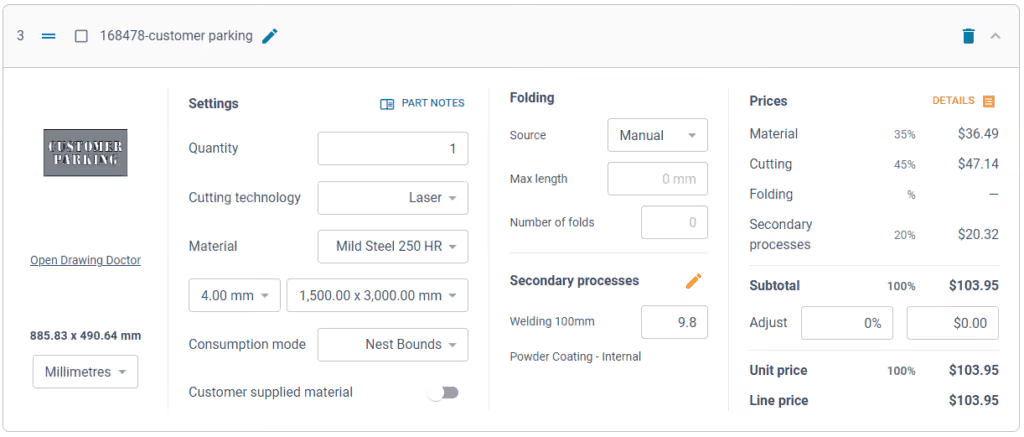
“In addition to providing quotes in minutes, Tempus Tools can also produce production documents with the click of a button, to add further efficiency to running a job shop floor,” he adds.
A shift in the industry
With customers demanding faster service, the industry is shifting to tailored laser cutting quoting solutions, to enhance their RFQ response times, and Mark sees this as part of a larger global trend.
“It’s evident across a number of industries – smarter players want to utilise technologies specifically targeted to their industry to out-pace competitors. And laser cutting job shops are enthusiastically getting on board with this trend,” he says.
“Tempus Tools has been specifically designed for laser cutting job shops. It’s quick to set up, intuitive, and user-friendly, so the entire team can use it with minimal training, instead of relying on one specialist.”
Tempus Tools cloud-based laser cutting quoting software can be set up with information on material price, cutting time, labour, and other relevant information, to generate quotes quickly and accurately, with repeatability.
“The Tempus Tools team has decades of experience in the laser cutting industry, from the shop floor, through to management, and running their own laser cutting enterprises, so we know the industry inside out – and we can support through setup and every step of the journey, for no additional charges,” adds Mark.
“A major inhibitor of laser cutting quoting software has often been cost, with powerful software that can do it all costing thousands per month. But if you only need dedicated laser cutting quoting software, our plans start from US$100 per month, and are packed full of features you will actually use,” he says.
Switching software – overcoming challenges
Even with the knowledge of the benefits of dedicated laser cutting quoting software, job shops can be hesitant about the time involved in switching, says Mark. He notes some of the main concerns:
- Time – often job shops have tried other software implementations and it’s taken months, and they just cannot afford to spend that time again. But Tempus Tools isn’t like other software. For a job shop with one laser, press brake, and standard secondary processes, set up takes less than 90 minutes.
- Staff training – job shops often believe their staff don’t have the time or capacity to learn a whole new software. But again, Tempus Tools is different. It’s designed to be user-friendly, easy to learn, and staff end up doing their jobs more efficiently, and enjoying the features right away.
- Hidden costs – this is a big factor for any software, and job shops are highly alert to cheap upfront costs, followed by lots of add-ons. No one likes to be “nickel and dimed”. For Tempus Tools, it’s a monthly or yearly subscription, and that’s all. No extra charges for support, upgrades, or training. Features all have a set pricing that’s clear from the outset.
- Too many programs – some job shops have two, three, or more different software programs – why add more, especially if they don’t talk to each other? That’s a totally valid concern. Tempus Tools outputs a CSV as standard with all the quote data, making integration seamless and easy.
“The Tempus Tools leadership team has decades of experience working from the shop floor to the top floor, so they understand the pain of changing software, and have designed Tempus Tools to be effortless and simple,” says Mark.
Tempus Tools features
Tempus Tools features that have been specifically designed for laser cutting job shops include:
- 3D model extractor. Identify, extract and unfold sheet-metal parts directly from 3D assemblies without a 3D software package.
- PDF to CAD convertor. Convert a vector PDF into a CAD file instantly. No tracing, no CAD package, just click on a part and extract it into your quote.
- Tube quoting. Easily drag and drop rectangular, square or round hollow sections into the tube module. It quickly calculates highly accurate cutting time and material consumption for pricing.
- Web Store. Let your customers get instant pricing and place orders from your website 24/7 with an online quoting portal.
- Secondary processes. Get accurate and consistent folding prices quickly using the built-in folding algorithm developed by specialists with decades of experience using brake presses.
- Drawing Doctor®. Upon upload of a 2D DXF or DWG file, Drawing Doctor® automatically corrects for double lines, dimensions, and small end points that are hidden in some drawings.
- Part Library. Part Library allows you to save parts that you’ve produced for a customer for re-use. Saves time on repeat orders and quotes, by dropping an existing part straight into the quote, ready to calculate, based on the latest pricing.
“These are just a few of our most popular features, but there are lots more within Tempus Tools, and our development team is constantly listening for customer feedback to determine what new features can be added,” says Mark.
“So for effortless laser cutting quoting, don’t let software hold you back, let it be the catalyst that drives business growth. We offer an obligation-free trial of Tempus Tools so that laser cutting job shops can see the difference for themselves.”
Read blog
Guides
0
min read
How to set laser cutting prices that are both competitive and profitable
Metal fabrication and laser cutting job shop owners have all asked themselves at one point, “how should I set my prices?”.
It’s a delicate balance. Set your prices too high and customers may walk away to the competition, but set your prices too low, and you may be working too hard for little or no profitable return.
Setting a baseline
“The first thing to do is understand all of the costs that are associated with running your laser machine. Once you have a complete overview, best practice is to apply a full absorption costing method to your business,” advises Bruce Thomas, Product Executive at Tempus Tools. Bruce has decades of experience in the laser cutting industry. His experience is complemented by the Tempus Tools team, which are highly knowledgeable in the laser cutting industry, with practical, hands-on experience on the shop floor, through to management.
“Full absorption costing means that you’re absorbing overhead costs into the hourly rate. In laser cutting job shops, this could be direct costs, like labour, as well as indirect costs like rent, insurance, power, and maintenance. But each case is different, so we can provide guidance on how to perform this type of calculation,” he says.
Bruce explains that once you have calculated all the costs within a job shop and created an annual figure, you can set an accurate yearly revenue target, which can be broken down into monthly and daily objectives. This breakdown is an effective way to focus on revenue goals for the job shop.
“This data should give you an idea of what prices need to be set in order to be profitable, but you won’t know if they are exactly right until you get market feedback, so be prepared to adjust these initial prices,” says Bruce.
A word on assumptions
Full absorption costing is a great starting point, but Bruce points out that this calculation does require some assumptions, such as the number of hours the shop will be operational for, and the percentage of those hours the machine will be cutting (known as the utilisation rate).
“Varying the utilisation rate can have a big impact on how costs are distributed. If your machine isn’t running for as many hours per day as you predicted (actual cutting time), then you find yourself in a situation where you’ve priced your cutting service too low,” he says.
“In other situations, you might increase the number of shifts per day, or add shifts on weekends, which can increase efficiency without changing fixed overheads, resulting in a more competitive hourly rate.
Getting ahead and staying competitive
“Of course, once you’ve come up with a price, it’s crucial to see if it’s competitive with the market, and one of the best ways to do this is to use software to monitor your win/loss ratio,” he says.
“A typical win/loss ratio is about 30-40%. This means, for every 100 jobs you quote for, you win 30-40 of them. Lower than 30 means the pricing is too expensive and you’re losing work to competitors, and above 40 means the pricing is too cheap, meaning you are doing a lot of work for a lower profit margin.”
“It’s important to monitor pricing over time, and see how it changes in reaction to trends, too. For example, material price fluctuations or changes in demand from different industries will have an impact on pricing.”
“Similarly, technology changes will have an impact. Cheaper and more powerful machines, and more automation will allow more advanced laser cutting tasks to be done with lower costs.”
“It’s important to know your customer, but it’s equally important to know your competitor and what they are offering, and for how much.”
Hourly rates only go so far
Much of the metal fabrication and laser cutting industry uses hourly rates to calculate a price, which is then quoted to customers, but this only works up to a point, says Bruce.
“To remain competitive, you need to keep monitoring prices. Each quote – regardless of who prepares it – needs to be consistent and accurate. One of the best ways to do this is to use laser cutting quoting software, so that any changes are implemented within the software, rather than on a per-quote basis,” he explains.
There are a range of factors that can affect a quote, and it can often mean one job shop will quote at a different rate to another. Bruce explains that this can be for reasons such as:
- The speed and size of the machine. A 6kW laser cutting machine can vary from approximately $180,000 to $1,200,000, which is a huge difference. Each machine will perform at different speeds, and allow different levels of sophistication.
- Whether the machine is paid off or not. If it’s still not paid off, this might have to be factored into the hourly rates.
- Cutting thickness, with thicker cuts demanding higher costs.
- Cut quality – all machines will be able to produce an acceptable quality, but some customers may demand an additional level of precision and finish, and if this takes additional time, it will need to be considered in the costs.
“With all that being said, your customer is buying on a per-part basis. They are comparing your part priced at $10 with the competitor’s part priced at $8. So, you need to adjust for this difference using software and data, rather than relying solely on a ‘gut feeling’. Knowing your bottom line gives you the confidence to accept or reject the work,” he says.
Added value wins more jobs
Once you’ve figured out a price, to really stand out from the competition, it’s all about the added value you can deliver, says Bruce.
“Consider your delivery times, customer service, expectations management, and understanding a customer’s unique needs. Do they need all their parts individually packed and labelled, for example? If you can meet their needs, you’re more likely to win the job,” he says.
“Adding value is always better than discounting price. In a race to the bottom on price, nobody wins.”
Tempus Tools helps win more jobs
To help deliver added value, monitor win/loss ratios, and provide faster, more accurate, and more consistent quotes, Tempus Tools created Tempus Tools. Tempus Tools is multi-functional laser cutting quoting software that is calculation-based and runs on a Software as a Service (SaaS) model. It can be set up with information on material price, cutting time, labour, and other relevant information, to generate quotes quickly and accurately.
“Tempus Tools can give job shop owners more accurate estimates of time, which leads to greater consistency,” says Bruce.
“Additionally, Tempus Tools can generate printable part labels, and produce work orders with times listed on each task. Tempus Tools provides consistent and accurate data on folding, cutting, and secondary processes, so that quotes to customers are exactly right.”
“We’ve helped a huge variety of different job shops with full absorption costing, win/loss ratios, setting up pricing, and then generating fast and accurate quotes – so if you’re looking to optimise your job shop’s operations, we’re here to help,” he concludes.
Read blog

Articles
How to Buy Steel for a Fabrication Shop: Suppliers, Stock, Freight and Margin
What to forward-buy, what to buy as needed, how to work with steel suppliers, and how buying decisions show up in your quotes.
How you buy steel decides more than what's on the racks. It sets your cash flow, how fast you can quote an urgent job, and how much margin is left when the job ships. The gap between when you pay your steel supplier and when your customer pays you is at the heart of any good steel buying strategy.
This guide covers what to forward-buy and what to buy as needed, how to work with steel suppliers, freight and delivery, and how buying decisions flow into your quotes.
Plan purchases around a bell curve
Not every material deserves the same buying approach. Picture your consumption as a bell curve. It usually comprises:
- The middle: mild steel from 2 or 3 mm up to 12 mm. This is the bulk of most shops' work. Forward-buy it.
- The thin end: cold rolled and thin sheet. Buy as needed, even if small quantities mean you have to use different suppliers.
- The thick end: 16, 20 and 25 mm plate. Top up monthly, and add a few sheets to each bulk order.
- Stainless and aluminium: buy project by project, but keep a minimum range on hand.
In most job shops mild steel is around three-quarters of material use, with stainless and aluminium making up the rest. Shops in coastal or tropical areas can run much higher on stainless and aluminium. You'll want to understand what you're currently using and the positioning of your business when you make your own bell curve.
Forward-buy the middle of the curve
For the mild steel you know you'll use, the cheapest and safest approach is to forward-book it.
Work out what you'll consume over the next three months. Say it's 30 tonnes across 3 to 12 mm. Place one order for the full 30 tonnes, delivered 10 tonnes a month. You take every delivery regardless, because hot rolled mild steel doesn't spoil and you know it will get used.
Booking 90 days out means you're buying January's steel in October. Your supplier rolls your order in with its other customers' forward orders and buys from the mill on those projections. That volume predictability helps you get lower prices.
Two rules:
- Only forward-buy hot rolled. Cold rolled comes sealed and starts to rust once the pack is opened, so buy it when a job needs it.
- Time orders to your billing cycle. For example, if you place the month's order late in the month and ask for it to be invoiced and delivered on the 1st, it becomes a regular feature of your monthly profit and loss statement. That makes your accounts easier to manage and shows you more clearly what's happening in the business.
Top up thick plate with your bulk orders
Thick plate moves slowly and ties up a lot of money per sheet. Top it up monthly rather than stocking deep.
When the bulk truck is coming anyway, add a couple of sheets of 20 and 25 mm. It builds the load towards the tonnage that gets you the best freight rate, and keeps you covered for the next heavy job.
Stainless and aluminium: carry a minimum range
Stainless and aluminium are usually bought per project. Still keep a small range in common grades and thicknesses, such as 316 and 304 stainless and 5005, 5052 and 5083 aluminium. If one item is a steady seller, buy it by the pack. One Tempus Tools customer, who runs a small single-laser shop, buys 3 mm 5005 aluminium by the pack because local customers keep ordering it for ute canopies and doors.
Be careful with expensive thick stainless. A full sheet of 25 mm 316 can take a long time to use up. The alternative is to buy only the piece you need. Many suppliers will cut a 1200 x 1500 mm piece from a plate and sell you that.
What carrying stock costs
Stock is money sitting on the floor. That same single-laser shop carries around $160,000 of material and turns it over about eight times a year. They'd like it to turn faster, but in a regional town the stock is what lets them take urgent work. When a boat is stuck waiting on a 316 stainless part, the customer can't wait days for material to arrive from the city, and they'll pay a premium to get it now. That premium only exists if the material is already on the rack.
Build relationships with steel suppliers
Price matters. As one shop owner put it, "$50 a tonne is $50 a tonne." Let suppliers know they have competition.
But spreading your buying across every supplier in town costs you something price can't buy back. A supplier you buy most of your steel from will extend your terms an extra 30 days in a tight month, and will find 5 tonnes of 25 mm and get it on the truck when you need it in a hurry.
A practical setup is one principal supplier for the bulk of your tonnage, with a smaller share to a local supplier for convenience and top-ups. When a competitor offers you a lower price, take it to your main supplier: "I've been offered $50 a tonne less, but I'd rather stay with you." More often than not they'll meet you, or meet you halfway.
Watch suppliers who start cutting
Some steel service centres add laser cutting. When they do, they can price their cut parts on what the steel costs them, while you're paying their price plus your margin. If you buy at $1,550 a tonne and add 20%, your material is in the quote at $1,860 a tonne. Theirs goes in at $1,550. Know which of your suppliers are also your competitors, and don't build your whole supply around one.
When going direct to the mill makes sense
Buying direct from the mill needs serious volume and cash. A container-sized commitment can run to $300,000 of steel. Letters of credit can help with payment, but you still need to sell it all. For most job shops, a good service centre relationship is the better deal.
Minimum order quantities and part sheets
Service centres will sell you part sheets, down to a quarter sheet. You pay for that convenience, because the supplier has to cut it and keep the offcut. Before buying a part sheet for a one-off job, compare the price per kilogram with a full sheet, and be honest about whether you'll use the rest. Stock that sits for a year isn't a saving.
If you sell part sheets or offcuts to your own customers, price them as a cut part, not raw material. Charge as if you'd cut the rectangle, and put a proper margin on the material.
Freight, mixed loads and delivery
Freight changes the economics of every order, especially outside the big cities.
- Build full loads. Bulk mild steel arrives most economically as a full truck. Mix in thick plate, stainless or aluminium to reach the tonnage.
- Compare all-up prices. In regional areas, local suppliers bring their steel up from the same city you would. Once freight is included, buying direct from a city service centre and buying locally often land at the same price per tonne.
- Set pack weights. Tell your supplier the maximum pack weight you can unload. If your forklift is rated at 2.5 tonnes, ask for packs of 2 tonnes or less.
- Rotate stock as it lands. Put new deliveries under existing stock so the oldest material is used first. Keep thick plate (12 mm and up) in floor bays and lighter packs on the first beam level. Our guide to sheet metal racking and storage covers the layout.
Keep material certificates with the batch
Every delivery comes with a heat number and material certificate. Using stock first in, first out keeps those certificates matched to the sheets you're cutting. The best practice is to record the certificate against each nest, so a question about any part can be traced back to the batch it was cut from.
Buying steel for quick-turn jobs
Urgent jobs are where buying and quoting collide. If the material isn't in stock, the quote depends on the supplier's lead time, freight and any rush charges, and on whether a substitute grade is acceptable to the customer.
Price that in from the start. A customer with a machine down will pay for speed. Quote a premium on the cutting and on the material, and only promise a date once the supplier has confirmed the stock. Some shops take this further and run a second Web Store under a separate brand for rush work, with higher pricing than their main store.
How steel buying affects quoting and margin
Material is usually the biggest part of a laser cutting quote, so buying decisions show up directly in your margin. The real cost of material in a job includes:
- The price per tonne you actually paid
- Freight, rush charges and minimum order costs
- Offcuts and scrap, less what you get back for the scrap
- The cost of carrying stock until it's used
A healthy material margin on mild steel is around 20%, measured after scrap. Work it out as material revenue plus scrap revenue, minus what you paid for the steel.
That margin only holds if the prices in your quotes are current. If steel goes up $100 a tonne and your price list doesn't, every quote you send gives away margin. Our guide to how material prices affect laser cutting jobs shows how quickly it adds up. A steel weight calculator helps check what a part or sheet should cost by weight.
Common mistakes when buying steel
- Leaving it to the last minute. Poor planning is the biggest one. A rush order means no time to negotiate, and the material price eats the profit on the job.
- Chasing the cheapest supplier every time. You save a little per tonne and lose the relationship that gets you credit and urgent stock.
- Forgetting freight. The cheapest price per tonne isn't the cheapest delivered.
- Over-buying for one-off jobs. A full sheet of expensive plate for a single part ties up cash for months.
- Forward-buying cold rolled. It rusts once the pack is opened.
- Quoting before confirming stock. The price and date both change if the material isn't there.
- Stale prices in quotes. Steel prices move, and old prices quietly cut your margin.
Keep material prices current in your quotes
Buying and quoting are one process. The supplier relationship gets you a fair price. Your quoting system has to carry that price through to every job.
Tempus Tools keeps material prices in one place. Update a price once and every new quote uses it. Material sits alongside your machine rates, cutting and secondary processes in the same pricing rules, so the whole job is priced the same way whoever does the quote. See how it works for fabrication shops, job shops and sheet metal shops, or read more about fabrication estimating software.
Negotiate, and pick a principal supplier
Buying steel well isn't about the lowest price on every order. Forward-book the steel you know you'll use, keep a lean range of the rest, build loads that make freight worthwhile, and give most of your business to one supplier who'll look after you when it counts. Then make sure your quotes use what the steel actually costs.
The advice from one long-time shop owner was simple: "Negotiate, negotiate, and have a principal relationship."
Frequently asked questions
How do fabrication shops buy steel?
Most shops buy from a steel service centre. Mild steel that's used every week is forward-booked, often 90 days out with monthly deliveries. Thick plate is topped up monthly. Cold rolled, stainless and aluminium are bought as jobs need them, with a small range kept in stock for urgent work.
What should you check before buying steel for a job?
Check the grade, thickness and sheet size the job needs, whether you already have it in stock, the supplier's lead time, and the delivered price including freight. For one-off jobs, decide whether a part sheet or cut piece is cheaper than a full sheet you may not use.
What is a minimum order quantity when buying steel?
It's the smallest amount a supplier will sell. Service centres will usually sell part sheets, down to a quarter sheet, at a higher price per kilogram. Mills and bulk deals need much larger orders. Buying more than a job needs ties up cash in stock that may sit for months.
How do freight costs affect steel buying?
Freight can decide which supplier is cheapest. A full truckload carries the best rate, so shops add thick plate or other materials to reach the tonnage. In regional areas, local suppliers pay the same freight from the city, so the delivered price per tonne often ends up the same.
Is it better to buy steel from one supplier or multiple suppliers?
Most shops do best with one principal supplier and a smaller share to a second. Concentrating your volume gets you better prices, extended terms in a tight month and priority on urgent stock. Keeping a second supplier gives you a price check and a backup.
How does steel pricing affect fabrication quotes?
Material is usually the largest cost in a laser cutting quote. If steel prices rise and your quoting prices don't, every quote gives away margin. Keep material prices current, include freight and scrap in the cost, and price urgent jobs with a premium on material as well as cutting.
See how Tempus Tools helps fabrication shops quote with current material costs and consistent pricing rules, or book a demo.
Read blog
Articles
Machine Shop Insurance: What Fabrication Shops Should Know About Coverage, Risk and Downtime
The cover fabrication and machine shops should think about, how to insure machines at the right value, and how to review your policy each year.
Machine shop insurance is more than a policy you renew without reading. A fabrication shop has expensive machines, flammable dust, heavy material, customer parts on the floor and deadlines that don't move when a machine stops. The right cover depends on what would actually hurt your business if it went wrong.
This guide covers the main types of cover, the decisions shop owners get wrong, and how to review your insurance each year. It applies to shops in the US, UK and Australia, though policy names differ between countries. It isn't insurance advice. Every shop's policy should be set with a qualified broker or insurer.
Why machine shops need insurance
Most of a fabrication shop's value sits in a few machines. A laser, a press brake and the compressor and extraction that support them can be worth more than everything else in the building. Losing one to fire, damage or breakdown stops production, and the bills keep coming while it's stopped.
The risks are specific to the work:
- Fire in extraction systems and dust collectors
- Injuries from sheet edges, heavy plate, forklifts and press brakes
- Theft of tooling and stock
- Damage to customer parts and materials while they're in your care
- Lost revenue while a machine is down
Common types of machine shop insurance
Exact policies and names vary by country and insurer, but the main types are:
- Commercial property insurance. Covers buildings, contents, machines and stock against fire, theft, storm and similar events. Often sold as part of a business owner's policy (US) or a general business package (UK and Australia), sometimes bundled with cover for cash on the premises and employee fraud.
- General liability (public liability in the UK and Australia) and product liability. Covers claims from injury or damage caused by your business or the parts you supply.
- Workers' compensation (US and Australia) or employers' liability (UK). Covers staff injured at work. Compulsory for most employers in all three countries, and usually a separate policy.
- Business income (US) or business interruption (UK and Australia). Pays ongoing costs and lost margin while the business can't trade after an insured event.
- Equipment breakdown (US) or machinery breakdown (UK and Australia). Covers repairs, and sometimes lost revenue, when a machine fails mechanically or electrically.
- Commercial vehicle insurance. For delivery trucks and vans.
Property cover usually protects against external events like fire or theft. It won't pay when a machine simply breaks down. That needs equipment breakdown cover.
Equipment breakdown cover: a judgement call
Equipment breakdown insurance (called machinery breakdown in the UK and Australia) pays for repairs and, depending on the policy, the revenue and overheads you lose while the machine is down. It isn't cheap, and some experienced shop owners avoid it, because the payout terms can be opaque and hard to argue.
Whether it's worth it depends on how well you can recover on your own. A large shop with its own maintenance engineers and spare parts can often get a machine running again quickly. A small shop with one laser, no in-house engineer and no spares has nothing to fall back on. For that shop, a major breakdown can stop all cutting for weeks.
Plan for parts, not just the policy
Getting parts can matter more than paying for them. Some of this varies by laser brand, and by the extent of local support in your region.
One Tempus Tools customer we spoke to knew buying a Chinese laser was risky from this perspective. They found a brand where most of the laser was standard parts: sensors and components that could be sourced from many suppliers. The exception was the laser source and the cutting head. So they purchased a spare cutting head with the laser. It's often a better hedge against downtime than a breakdown policy.
Insure at the right value
The most common mistake is insuring machines for the wrong amount.
Don't over-insure lasers
Replacement cost cover (called new-for-old in the UK and Australia), which pays to replace a machine with a new one, is expensive. Many shops insure machines at their current value instead, called actual cash value in the US and indemnity value in the UK and Australia. Laser prices have dropped a long way, so a machine's current value and its replacement cost both fall over time. If you don't lower the insured value at each review, you're paying premiums on value that no longer exists.
Don't under-insure press brakes
Press brakes are the opposite. A well-serviced press brake holds its value for years. One shop paid around $350,000 for a press brake that would still sell for about $250,000 with its tooling, while its depreciated book value was closer to $150,000 to $180,000. Insuring it at book value would leave a large gap if it were destroyed.
Under-insuring can also cut your payout on smaller claims. Most property policies include a clause that reduces any claim in proportion to how far you're under-insured. It's called a coinsurance clause in the US and an average clause in the UK and Australia. If your assets are insured for half their value, a partial loss may only be half paid.
Look at what each machine would cost to replace on today's market, not what the depreciation schedule says.
Fire risk in fabrication shops
Machine fires are rare, but when they happen they're serious, and fire is where under-insuring hurts most.
The risk is in the dust. Cutting several materials on one laser puts mixed dust into the extraction system. Fine aluminium dust mixed with mild steel dust can ignite from a spark, and can explode. A strong filtration system on the extraction helps, along with keeping it clean.
Linishing and sanding are a classic source of fires. A belt used on mild steel and then on aluminium can start one. Keep separate belts for each material and use the right dust controls.
Tell your insurer what materials you process and how your extraction is set up. It affects your risk, and an insurer that doesn't know may dispute a claim.
Liability risks
Liability cover protects you when someone else is hurt or suffers a loss because of your business. In a fabrication shop that can include:
- A visitor or delivery driver injured on site
- Work done at a customer's site, such as measuring or installation
- A part you supplied failing in use and causing damage or injury
- Damage caused during delivery
Check what your policy covers for parts you make to a customer's drawing, and for work you subcontract to someone else, such as powder coating.
Customer materials and property
Shops often hold customer-supplied material, part-finished assemblies and parts waiting for collection. If a fire or theft destroys them, you may be liable.
Many general business policies don't automatically cover goods that belong to someone else. Ask your insurer how customer property is treated and whether you need to declare its value. Clear job records help here. If you know what was on site, whose it was and what it was worth, a claim is much easier to support.
Business interruption insurance
Business interruption cover keeps the business alive after an insured event. Your rent, loan repayments and wages continue whether or not the building has burnt down.
Claims are usually assessed on the margin you would have earned: what each job contributes after direct costs, which pays your overheads. Insurers call it gross profit in the UK and Australia, and business income in the US. So insure for the margin you need to cover fixed costs while you rebuild, and allow enough time to get machines replaced and running.
Part of recovery is getting your records back. When quotes, drawings and customer details lived in filing cabinets, a fire could wipe them out. Cloud systems have made that much easier. You still need to check that your quoting, job and accounting records are stored somewhere a fire can't reach.
Insurance for small machine shops
Small shops feel insurance decisions more:
- One or two machines may carry the whole business, so a single breakdown stops everything
- Cash reserves are thinner, so the deductible (excess) and the wait for a claim hurt more
- There's often no in-house engineer or spare parts
- The owner is usually also the estimator, operator and bookkeeper
For a small shop, business interruption cover and a plan for critical spares deserve as much attention as the property policy. For scale, one Tempus Tools customer running a small single-laser shop in Australia pays A$1,500 to A$2,000 a month for insurance, excluding workers' compensation.
Review your insurance once a year
Treat insurance as an annual business review, not an automatic renewal. A practical rhythm:
- Start six weeks before your policy renewal.
- Look back at the year: revenue, contribution margin, what you bought and sold, and any incidents.
- Project the next year: new machines, more staff, new processes, different materials.
- Update the insured value of every machine to today's market value.
- Set business interruption cover to match the margin and overheads you'll need to cover.
A clean claims history makes insurance easy to buy. Some businesses try to claim back their premium every year. As one shop owner put it, insurance is "just the cost of doing the job."
Questions to ask your insurer
- Are my machines insured at current value or replacement cost (new-for-old), and what does each cost?
- Does my policy cover equipment breakdown, or only external events?
- How is a business income or interruption claim calculated, and for how long will it pay?
- Is customer-supplied material covered while it's on my premises?
- What does product liability cover for parts made to a customer's drawing?
- Is there a coinsurance or average clause, and am I insured for enough to avoid it?
- Is subcontracted work, such as powder coating, covered?
- Are deliveries and goods in transit covered?
- What do you need to know about my extraction systems and the materials I cut?
- If I rent the building, what is my responsibility and what is the landlord's?
Keep job records organised
Insurance covers the cost after something goes wrong. Good records make recovery faster and claims easier to support.
When quotes, drawings, customer requirements and job details sit in one system, you know what was in progress, whose material was on site and what each job was worth. Tempus Tools keeps the whole job in the cloud, from the first RFQ and estimate through to production documents. Integrations pass the same information to your accounting system. See how it works for machine shops, fabrication shops and job shops.
Review your cover with a professional
Machine shop insurance protects you against the events that could close the business: fire, theft, injury claims and long stoppages. The right cover depends on your machines, your materials, your size and how well you can recover on your own. Review it every year, insure each machine at what it's really worth, and talk it through with a qualified broker.
Frequently asked questions
What is machine shop insurance?
It's the set of policies a machine or fabrication shop uses to protect itself. That usually includes property cover for buildings, machines and stock, general (public) and product liability, workers' compensation and business interruption. Some shops add equipment breakdown cover. The right mix depends on the shop, so set it with a qualified broker.
What types of insurance do machine shops need?
Most shops look at commercial property insurance, general (public) and product liability, workers' compensation or employers' liability, business interruption and vehicle insurance. Equipment breakdown cover is optional. Requirements vary by country, and cover for injured staff is compulsory for most employers in the US, UK and Australia.
Does machine shop insurance cover equipment breakdown?
Usually not. Property policies cover external events like fire, theft and storm damage. Mechanical or electrical failure needs separate equipment breakdown cover (machinery breakdown in the UK and Australia), which can pay for repairs and, depending on the policy, lost revenue while the machine is down.
Does machine shop insurance cover customer materials?
Not always. Many policies don't automatically cover goods that belong to someone else. Ask your insurer how customer-supplied material and parts are treated while they're on your premises, and whether you need to declare their value.
What is business interruption insurance for a machine shop?
It covers ongoing costs and lost margin while the shop can't trade after an insured event, such as a fire. In the US it's usually called business income cover. Claims are based on the margin you would have earned, so the cover should be enough to pay rent, wages and other fixed costs until you're running again.
See how Tempus Tools keeps quoting, job information and production documents organised from RFQ to production, or book a demo.
Read blog
Articles
Fabrication Shop Layout: How to Plan a More Efficient Metal Fabrication Workflow
How to plan a fabrication shop floor around the way work moves, how much space machines and storage need, and the layout mistakes that slow production.
Getting the layout of your fabrication shop correct is critical to your efficiency and profitability. How far every sheet travels, how often the forklift moves and how long a job waits between machines are all determined by layout. Do it well and work moves in one direction with little handling. Do it badly and you pay in walking, double handling and bottlenecks every day of operation.
This guide covers how to plan a sheet metal fabrication shop layout based on internal workflow, how much space machines and storage need, and tips to avoid the layout mistakes we see most often.
Why fabrication shop layout matters
Most of the cost of a poor layout is time nobody records. An operator crosses the shop to find material. The forklift goes the long way round the laser. Parts sit beside the press brake because nobody knows they're there. Each delay is small, but they can slow every job.
Layout also locks in costs that are hard to change later. Power, gas lines, extraction and racking are expensive to move once they're installed, so the layout needs planning before the machines arrive.
A good layout:
- Moves work in one direction, from receiving to dispatch
- Keeps material close to the machine that uses it
- Gives forklifts and people separate, clear paths
- Keeps welding and grinding away from the laser
- Lets the office see both the production floor and the front counter
Start with the way work moves through the shop
Plan the layout around the path of a job. The target is a one-directional flow, where work never doubles back on itself.
In a laser-based fab shop, the sequence usually runs:
- Receiving
- Material storage
- Laser cutting
- Sorting, where parts come off the skeleton and go into parts racks
- Press brake
- Welding bays
- Linishing, finishing and inspection
- Packing and dispatch
Not every job uses every step. Laser-only parts sometimes skip folding and welding and go straight from sorting to packing.
The flow doesn't have to be a straight line. A U-shaped flow is still one-directional, and it brings finished work back to where material came in. Receiving and dispatch can then share one area: trucks use the same door, the forklift works one apron, and you don't give up floor space to two loading zones.
How much space a fabrication shop needs
As a planning example, a shop with one laser, a press brake, three welding bays, material storage, finishing and an office needs at least about 1,600 m² (17,000 sq ft). Here's how the main areas add up:
| Area | Space allowance | Notes |
|---|---|---|
| Laser and working area | 14–15 m x 12 m, about 160–200 m² (46–49 ft x 39 ft) | Forklift access on both sides, room for a transfer table |
| Sheet storage | At least as much as the laser, often more | Depends on stock levels and racking type |
| Press brake | 6 m (20 ft) clear in front | Forklift access at both ends and behind |
| Welding bays | 8 m x 10 m each (26 ft x 33 ft), about 240 m² for three | Fume extraction over every bay |
| Forklift aisles | 4 m (13 ft) wide | Allows for the tines and overhanging plate |
| Pedestrian walkways | 1.5 m (5 ft) wide | Marked crossings where they meet forklift lanes |
Draw each area as a block to scale, in CAD or as paper cut-outs on a floor plan. Place the blocks in process order, then draw the forklift lanes and walkways around them. Moving a block on paper costs nothing. Moving a laser costs a lot.
Material flow and storage
Material storage sits straight after receiving and right beside the laser. The laser should be:
- Next to sheet storage
- Close to the receiving bay
- Reachable by forklift from both sides
- Laid out with room for a transfer table, unless a tower or other automation loads it
Allow at least as much floor area for racking as for the laser, and often more, depending on how much stock you carry and how efficiently you store it. Use rollout cassette racks for sheet, not pallet racking, and cantilever racks for tube and long product. Our guide to sheet metal racking and storage covers the options.
Handling time is part of the cost of every job. If a sheet takes 15 minutes to find and load, that time comes out of your hourly rate whether you quote for it or not.
Plan for the forklift
The forklift moves most of the material in a fab shop, so give it room. Forklift aisles should be 4 m wide. The common mistake is forgetting the tines, especially extended tines, and the plate hanging off them. Allow space for the forklift to turn into the racks and get around both sides of the laser. Our article on forklift theory covers parking, access and safety.
Consider an overhead crane
An overhead bridge crane can cut out many forklift moves, particularly around welding and assembly. It spans the width of the building on rails that run along its length. Beside the laser, a swing (jib) crane with a vacuum lifter is the usual way to load sheets. Crane operator licensing depends on where you are and the crane's capacity and controls, so check the rules before choosing one.
Machine placement and production flow
Press brake: next to the laser
The press brake comes straight after the laser in the process, so keep it close. Short walks and short forklift moves save time on every bent part. In a smaller shop it also means one operator can run the press brake while the laser cuts.
Give the press brake forklift access at both ends and behind. You need about 6 m clear in front, enough for a forklift carrying a 3000 x 1500 mm (10 ft x 5 ft) sheet. Don't put it against a wall. You rarely work from behind a press brake, but when you do, usually for maintenance or a particularly complex part, a wall stops the forklift getting in. Our sheet metal bending guide covers the process side.
Welding bays
A welding bay needs about 8 m by 10 m. Each bay needs fume extraction overhead, and so does any area where you linish or grind. Keep welding, grinding and linishing well away from the laser, because the dust they create contaminates it.
Make sure a crane or forklift can reach every bay. Large assemblies like ute canopies and truck bodies need lifting, and you don't want that done by hand.
Handheld laser welders are worth considering when space is tight. With some training, anyone with a steady hand can produce good welds. They need a protected area: screens around the work and a cover overhead. A dedicated room is better but expensive. Robotic laser welding only pays off with long-running jobs.
Finishing, inspection and packing
After welding, parts go to linishing, finishing and inspection, then on to packing beside dispatch. Keep packing close to the loading door so finished work isn't carried back across the shop.
Infrastructure: place the machine first
A laser needs gas, compressed air and power. If you run a nitrogen generator, plan where the compressor, generator, gas packs and oxygen supply will sit, and how the pipework reaches the laser. One Tempus Tools customer, who runs a small single-laser shop, keeps all of it outside the building, with piping down the factory to the machine.
Don't place the laser to suit the switchboard. Putting it near the power supply to save on electrical work is false economy. Lay the factory out the way it works best, put the laser where it fits that layout, and then pay for the cabling and pipework. As one shop owner put it, the inefficiency of running a shop without that planning is "diabolical."
Where to put the office
The office and admin area should be on the shop floor level, with a view of both the production floor and the customer-facing front of the business. As one shop owner told us: "Upstairs offices are a disaster."
In a square building, say 40 m by 40 m (130 ft x 130 ft), a good position is in the middle at the front. Customers see the office when they arrive, and windows at the back look out over production. Whoever runs the floor can see what's happening without leaving the desk.
Forklift and pedestrian traffic
Separate forklifts and people wherever you can. Keep forklift aisles 4 m wide and pedestrian walkways 1.5 m wide, with a marked crossing wherever the two meet. Many shops mark walkways in yellow and forklift lanes in green. Check the floor marking requirements under your local workplace safety rules.
Budget for upkeep. Forklift tyres and grit wear floor paint down quickly, and most shops need to repaint lanes every year.
Reducing bottlenecks between quoting and production
The layout moves material. Job information has to move too, and that's where many delays start.
Sorting is where the two meet. An operator pulling parts off the skeleton needs to know which go to the press brake, which to welding and which go straight to packing. If the part label or work order doesn't say, parts sit in the rack while someone walks to the office to ask.
The same happens when a job reaches the floor without:
- The current drawing revision
- Quantities for each part
- Material grade and thickness
- The processes each part needs
- The delivery date
Each gap means a trip to the office or a phone call. Fix the information flow and the physical flow speeds up with it.
Tempus Tools keeps the job together from the first RFQ and estimate through to production documents. An accepted quote becomes work orders and part labels that show each part's material, quantity and next process, so the floor works from the same information the price was based on, without anyone typing it in again.
Layout tips for small fabrication shops
Small shops have less space, shared work areas and a mix of jobs, and the same few people often quote, cut, fold and deliver. A rebuild usually isn't an option, but small changes can remove friction that repeats every day:
- Put the laser and press brake close enough for one person to run both
- Keep a linisher near sorting for laser-only parts
- Move the press brake off the wall if it's against one
- Stage tomorrow's material beside the laser before you go home
- Mark forklift lanes and walkways, even if it's only a few lines of paint
- Outsource welding if you can't build a safe bay with extraction
Moving into a bigger building
More space doesn't automatically make a shop more efficient. We've seen shops move into large buildings and get slower, because material, machines and people spread out and every trip gets longer. If you have more floor area than your work needs, block off the end of the building rather than spreading into it.
Shops running several lasers can lay out around material. Put thick mild steel, 12 mm and up, on a high-power laser, run thinner material on a faster machine, and keep stainless and aluminium on their own machines. Keeping aluminium and stainless away from mild steel also reduces contamination and the fire risk of mixed dust in extraction systems.
Automation is worth planning for, not necessarily buying. A storage tower beside a laser pays off for a shop running around the clock on repeat work. Automating retrieval from cassette racks with overhead cranes costs far more than it saves for most job shops.
Common fabrication shop layout mistakes
- Material storage far from the laser
- A press brake against a wall, with no forklift access behind it
- Forklift aisles sized for the forklift but not the tines or the load
- Welding and grinding close to the laser
- No extraction over linishing areas
- No staging area for the next day's material
- The laser placed near the switchboard instead of where the flow needs it
- An office upstairs, cut off from the floor and the front counter
- No marked walkways or crossings
- More floor area than the work needs
- Parts reaching sorting with no clear next step
Plan the flow before the floor
A good fabrication shop layout moves material and information in the same direction: receiving, storage, laser, sorting, folding, welding, finishing and dispatch, with the office able to see all of it. Size each area properly, give forklifts and people their own space, keep dirty processes away from the laser, and make sure every part reaches the floor with clear instructions.
See how it works for fabrication shops, job shops and sheet metal shops.
Frequently asked questions
What is a fabrication shop layout?
A fabrication shop layout is the arrangement of machines, storage, work areas, traffic lanes and offices on the shop floor. A good layout follows the path of a job, from receiving and material storage through cutting, folding, welding and finishing to dispatch, so work moves in one direction with as little handling as possible.
How do you plan a metal fabrication shop layout?
List every process in the order a job uses it, then work out the space each one needs, including forklift access. Draw each area as a block to scale in CAD or on paper, arrange the blocks in process order, and add 4 m forklift aisles and 1.5 m walkways. Place machines first, then plan power and gas around them.
What should be included in a small fabrication shop layout?
Receiving, material storage beside the laser, a sorting area with parts racks, the press brake close to the laser, a finishing area with extraction, packing and dispatch, and an office with a view of the floor. Small shops can share one area for receiving and dispatch, and often outsource welding when there's no room for a safe bay.
Why is material flow important in fabrication shops?
Every time material is moved, searched for or handled twice, the shop pays for time it can't charge for. Storing sheet beside the laser, keeping forklift paths clear and running work in one direction cuts handling time, reduces damage and keeps the machines cutting.
How does shop layout affect production efficiency?
Layout decides how far people and material travel and how often jobs wait. A press brake far from the laser, narrow aisles or storage on the other side of the shop all add minutes to every job. Over a year, those minutes add up to a large share of machine and labour time.
How can fabrication shops improve the handoff from quoting to production?
Make sure every job reaches the floor with the current drawing, quantities, material, processes and delivery date, and that part labels show where each part goes next. Generating work orders and labels from the accepted quote stops details being retyped or lost between the office and the floor.
See how Tempus Tools helps fabrication shops move from quote to production with clearer job information, or book a demo.
Read blog
Articles
Deburring Meaning: What It Is and Why It Matters in Metal Fabrication
What deburring means, why laser-cut parts have burrs, when parts need deburring, and how to price it as a secondary process.
Deburring means removing the burrs, sharp edges and leftover material that cutting, drilling, punching or machining leave on a metal part. It's one of the most common finishing steps in metal fabrication and laser cutting. It decides whether a part is safe to handle, ready to coat and easy to assemble, and it adds labour that has to be priced into the job.
This guide explains what deburring is, why burrs form, when parts need deburring and when they don't, and how to price it so it doesn't come out of your margin.
What does deburring mean?
Deburring is the process of removing burrs from a part after it has been cut, drilled, punched, machined or formed. A burr is a sharp edge, raised lip or small piece of unwanted material left on the edge of the part. Deburring leaves the edge clean and safe to handle, and ready for welding, coating or assembly.
You'll also see a few related terms:
- Deburr. The verb. A drawing might say "deburr all edges".
- Edge rounding. Going a step further than removing the burr, and giving the edge a small radius. Many deburring machines do both in one pass.
- Break sharp edges. A common drawing note asking for every sharp edge to be removed.
What are burrs?
Burrs are the rough material a cutting process leaves behind on the edge of a part. On laser and plasma cut parts, most of it is dross: molten metal that didn't clear the cut and solidified on the bottom edge.
On a laser-cut part, the two sides of the edge are different. Where the beam enters the sheet, you get a clean, sharp 90-degree corner. Where it exits, on the underside, you get the dross and the rough edge. How bad it is depends on the material:
- Aluminium. On a fibre laser you can get a good edge and still have a sharp burr hanging off the bottom. Some shops call them stalactites.
- Stainless steel. No matter how bright the cut edge looks, there's usually a thin, hard, black line of dross along the bottom edge.
- Mild steel. Heavy dross usually points to a settings problem: nozzle alignment, laser power or cutting speed. Oxygen-cut mild steel also has an oxide layer on the edge, which can affect how well powder coating holds.
Other processes leave burrs too. Drilling and machining raise a lip where the tool exits, punching leaves a burr on the die side, and shearing leaves a rough edge along the cut.
Why deburring matters in metal fabrication
Safety
A burr on a laser-cut part can cut open someone's hand. That might be your own staff sorting parts, or someone at the customer's site unpacking them. You don't want to be the shop that sent out parts that injured a customer's employee.
Coating and finishing
Customers most often ask for deburring when parts are going to be powder coated or anodised. Coatings don't hold well on sharp edges or loose oxide. Deburring and edge rounding remove both, giving the coating a clean, slightly rounded edge to grip.
Welding and assembly
Stainless and aluminium parts that will be welded need clean edges. Burrs also stop parts sitting flat or fitting together properly, which slows assembly and can cause rework.
Appearance
Anything decorative or visible, like a laser-cut screen, needs deburring. A rough edge is the first thing a customer notices.
Manual vs machine deburring
Manual deburring
Manual deburring uses hand tools: files, sanding discs, grinders, and pneumatic edge-trimming tools that run along the edge like a small router. A good edge-trimming tool leaves a smooth, rounded edge on aluminium and stainless.
Hand deburring suits small batches, one-off parts, bent or welded parts that won't fit through a machine, and edges a machine can't reach. For everyday laser work it's slow. As one shop owner put it: "If you try and do it manually, it's a very exhaustive process."
Machine deburring
A deburring machine uses abrasive belts, brushes or both to deburr and round edges as parts pass through on a conveyor. Parts come off the laser onto a trolley, get wheeled to the machine, and feed in on a roller conveyor. They travel through on the belt, and one person can load the infeed and unload the other side.
It's much faster than hand work, but it still takes labour. Someone has to feed every part and take it off again.
Deburring machines start at around $30,000. A high-end European machine can cost $100,000 or more. For a shop deburring most of its laser work, a machine is the only practical way to keep up.
High-volume shops may also use vibratory finishing or tumbling for small parts, where batches of parts are processed together in a drum or bowl of abrasive media.
Protective film
Stainless and aluminium sheet often arrives with a plastic film on one side. Ask the customer whether they want the film left on. If they do, deburr only the exit side, which is where the dross is, and leave the film on top. The top edge stays sharp, but it's clean. As one shop owner described it, "clean sharp, not dirty sharp."
When do metal parts need deburring?
For a quality product, almost always. Customers tend to ask for deburring only when they know coating or anodising is coming, but a sharp edge cuts whether or not the part is painted.
Parts that need deburring include:
- Laser-cut stainless and aluminium, especially if it will be welded
- Parts going to powder coating or anodising
- Decorative or visible parts, such as screens
- Parts people will handle, assemble or install
- Parts with mild steel dross from cutting
Parts that may not need it:
- Structural mild steel that will be welded, then grit blasted before galvanising or painting. The blasting cleans the edges.
- Parts the customer will grind or linish themselves during assembly
- Parts where the end use makes edge finish irrelevant and the customer has agreed to go without
One Tempus Tools customer, who runs a small single-laser shop, cut an $80,000 job of stainless ladders for a mining services customer. Deburring every part would have added about $10,000 in labour. The ladders were going into a marine environment, and the customer was going to grind the cut edges during assembly anyway. The shop deburred only the parts it had to break free or clean up, and quoted the rest without it.
The lesson isn't to skip deburring. Know your customer and the end use, and make it a deliberate decision on the quote.
How deburring affects quoting and job cost
Deburring adds labour, handling and sometimes machine time to every part that needs it. On the stainless ladder job, it would have added about an eighth of the job value. If that cost isn't in the quote, it comes out of the margin, or the parts go out with sharp edges.
The pressure to skip it is real. Deburring every part makes your price higher than the shop down the road that doesn't. The answer is to make the trade-off visible to the customer: deburred parts are the quality product, and parts without deburring come with sharp edges and a coating risk.
A practical approach is to include deburring on every quote as a visible line. The customer sees what they're getting and can ask for it to be removed. In our experience, few do. Some shops instead offer deburring as a selectable option in their Web Store, so customers choose it when they order.
Pricing deburring as a secondary process
Deburring is a secondary process, like bending, welding or powder coating, and it should be priced the same way: with rules, not guesswork. Factors that affect the cost include:
- Part quantity and size
- Material and thickness
- Total edge length and part complexity
- One side or both, and whether protective film stays on
- Plain deburring or edge rounding to a radius
- Machine or hand work, including parts too small or awkward for the machine
- Handling between the laser, the deburring station and the next process
Pricing it consistently means every estimator charges the same for the same part, and the margin holds on large jobs where the hours add up.
Tempus Tools lets shops set up deburring as a secondary process, priced from each part's properties, so it lands on the same quote as the cutting and bending. Once the quote is accepted, production documents show which parts need deburring, so the operator doesn't have to guess. See how it works for sheet metal shops and fabrication shops, or read more about fabrication estimating software.
Deburring is part of the job
Deburring is a simple idea: take the sharp edges off. But it decides whether parts are safe to handle, whether coatings hold and whether the customer sees a quality product. It also takes real labour. Price it into the quote from the start, decide deliberately when to leave it out, and make sure the floor knows which parts need it.
Frequently asked questions
What does deburring mean?
Deburring means removing burrs, the sharp edges, raised lips and leftover material that cutting, drilling, punching or machining leave on a metal part. The result is a clean, safe edge that's ready for handling, welding, coating or assembly.
Why is deburring important?
Deburring makes parts safe to handle, helps powder coating and anodising adhere to the edges, lets parts fit and weld properly, and improves appearance. Without it, sharp edges can injure staff and customers, and coatings can fail along the edge.
Is deburring done by hand?
It can be. Hand tools like files, sanding discs and pneumatic edge trimmers suit small batches and awkward parts. Most shops deburring regular laser work use a deburring machine, which processes parts on a conveyor with abrasive belts or brushes. It still needs someone to load and unload parts.
Do laser-cut parts need deburring?
Usually, yes. Fibre lasers leave a sharp burr on the bottom edge of aluminium and a hard black dross line on stainless, even when the cut looks clean. Mild steel needs less if the laser settings are right, but parts going to coating or handling still benefit from it.
Is deburring a secondary process?
Yes. Deburring is a secondary process that happens after the primary cutting or machining operation, alongside bending, welding, countersinking and coating. Like those processes, it adds labour and handling, and should be priced separately or built into the quote.
Should deburring be included in a fabrication quote?
Yes. Deburring takes labour and handling time, so leaving it out of the quote means either absorbing the cost or sending out sharp parts. Many shops include it as a visible line on every quote and let the customer ask for it to be removed.
See how Tempus Tools prices secondary processes like deburring alongside cutting and bending, or book a demo.
Read blog
Articles
Sheet Metal Racks: How Fabrication Shops Store and Handle Material
How fabrication shops store sheet and plate, which racking types suit which jobs, and why storage decisions affect production time and quoting.
Sheet metal racks look like a warehouse decision, but they shape how quickly a shop can find, load, stocktake and cut material. The wrong racking damages sheets, eats floor space and keeps the laser waiting between jobs. The right setup pays for itself faster than most owners expect.
This guide covers the main types of sheet metal storage racks, where each one fits, and the workflow decisions that matter as much as the racking itself.
Why sheet metal storage matters in fabrication shops
Walk into a job shop and the material storage tells you a lot about how it runs. Sheets left on the floor or leaning against posts are a warning sign. As one long-time shop owner put it: "Material not put away is a clear indicator of a very inefficient job shop."
Loose material costs money in ways that don't show up on a single invoice:
- Sheets on the floor get run over by forklift tyres and scratched by tines, and damaged sheets get scrapped
- Mild steel sitting on timber pallets rusts from the bottom up
- Operators lose time hunting for the right grade and thickness
- Loose sheets have sharp corners that someone has to steer around the factory
- Storage and forklift clearance swallow floor space you're paying rent on
We've seen shops in the US where stacks sit straight on the floor with junk piled on top of them, on the assumption that every stack is the thickness it's meant to be. In one, the material was stored outside under snow.
There's also a financial cost that owners tend to underestimate: the stock itself. One Tempus Tools customer, who runs a small single-laser shop, said they carried around 50 tonnes of sheet, worth roughly $130,000. They'd done the sums: to cover the cost of how it was stored and the rent they were paying, they'd need a material margin of around 25% instead of the 20% they charge, which would make them less competitive. The alternative is to close the gap through efficiency: more stock in less floor space, fewer damaging moves, and always knowing what's on hand.
Common types of sheet metal racks
Most fabrication shops use some mix of these:
Horizontal sheet metal racks: traditional pallet racking
The most common horizontal sheet metal rack in small shops is standard pallet racking, the same system warehouses use for boxes. Sheets sit flat on timber pallets, and the pallets sit on beams.
It's popular because it's cheap and quick to put up: bolt up the two end frames, drop the beams in between, and it's ready to load. The upfront capital cost is low.
The problems appear once you use it every day:
- The timber pallet takes up at least 100 mm of every bay before any steel goes on it
- Without a protective cover on the timber, the bottom sheet of mild steel rusts as moisture comes out of the wood
- Every beam and every bay has a load rating, so the heaviest plate (25, 20, 16 and 12 mm) has to go in the bottom bays whether that suits your workflow or not
- Pallets aren't solid, so a single sheet on a pallet leaves four sharp corners exposed while it's driven across the factory
Pallet racking can work for a shop just starting out. Most shops outgrow it.
Drawer-style sheet metal racks: rollout cassette systems
A rollout cassette system replaces timber pallets with steel cassettes that slide in and out of the rack on rollers, like large filing cabinet drawers. When a bundle of material arrives, you unpack it straight into a cassette. To use it, you pull the cassette out with the forklift tines, take it to the laser, lift sheets onto the bed with a vacuum lifter, and roll the cassette back into the rack. Nobody handles the sheets by hand.
For a small job shop, it's the clear choice. One shop owner who has run both systems put it simply: "You are better off by a country mile to have a rollout pallet system."
The advantages come from the design:
- No timber, so no rusted bottom sheets
- The material travels inside the cassette, protected, with no loose corners sticking out
- Each cassette carries far more weight than a pallet racking beam, so you can store more material, higher, in the same footprint
- Cassettes can be staged beside the machine for the day's work
That last point changes how the laser runs. At the start of the day, the operator pulls the cassettes for the day's jobs and stacks them within reach of the lifter. Each sheet goes from cassette to bed, and each empty cassette goes back to the rack with the next one already waiting. By the end of each day, the next day's work should be stacked up and ready to go.
A cassette system also puts a shop closer to automated material handling later, because the material is already in standard, machine-handled units.
What a rollout system costs and how fast it pays back
A cassette system for around 50 tonnes (three material types, two grades and a range of thicknesses) costs somewhere between $70,000 and $90,000. Payback is typically around 12 months.
The savings come from three places:
- Production time. A laser running two shifts with six material changes per shift makes 12 changes a day. At around 15 minutes each with poor storage, that's three hours a day the machine isn't cutting.
- Floor space. The small shop above uses 280 of its 650 square metres for material storage and the forklift space around it. Cassettes stack higher and need less clearance. At $150 per square metre a year, freeing up 80 square metres is worth $12,000 a year in rent, or room for a new process.
- Less damaged and scrapped material.
Vertical sheet metal racks
A vertical sheet metal rack stores sheets on edge in slots, like a toast rack. You can see every piece at a glance and flip through to the one you want, and the rack takes up very little floor space.
Vertical storage is best used for remnants, with full sheets kept flat. Full-size sheets are heavy and awkward to handle on edge, and standing them up and lifting them back out puts more strain on operators and more wear on the sheet edges.
Vertical racks work well with a strict remnant rule, covered further down: only store rectangles and squares, and label every piece.
Cantilever racks
Cantilever racks have a heavy upright column with arms that stick out from it, each engineered to carry a set load (up to around two tonnes). They're built for tube, bar and other long product. Flat sheet generally doesn't belong on them.
If your shop cuts tube as well as sheet, you'll likely need both: cantilever racks for long product and cassettes or flat racks for sheet.
Automated towers and storage systems
An automated tower sits beside the laser and feeds it. You load the tower's pallets, tell the system which sheet is in which pallet, and it pulls sheets, loads the machine and unloads cut parts. A tower needs floor space on its own, plus room around it to load it.
Towers are where we see the most money wasted. Shops buy one on the strength of a sales pitch and end up cursing the tower, when the real problem was buying it without understanding their own work mix. A fibre laser on thin material gets through sheets very quickly, and a tower only pays off when it's kept fed with the same few materials. If you're cutting one sheet of one thickness and then swapping the material in the tower for the next job, it isn't justified.
As a rule of thumb, you need to be running two shifts, and the tower should be close to dedicated to one material. A sensible split is to run only mild steel through the tower and cut all aluminium and stainless on a second machine without one. A single-laser shop turning over $2 to $3 million a year doesn't have the volume to justify one.
Towers also create a remnant problem. They don't load remnants well, because the machine can't easily orient an offcut with a cutout in one corner. Shops that run everything through a tower often stop saving remnants altogether. One Tempus Tools customer runs all its 6 mm and thinner material through a tower and charges for a full sheet even when a customer only needs a 500 x 500 mm part from 3 mm. That keeps the tower simple, but it means they rarely win small jobs.
At the top end are full automated storage and retrieval systems that run along a factory wall and deliver material to several machines with no forklifts involved. These can cost $750,000 to over $1 million. For a shop running 24 hours a day, six or seven days a week, they make sense. For anyone else, make sure the work and the contracts are in place first. There's nothing worse than a system that expensive standing idle, and anything mechanical can break down.
How poor sheet storage slows down quoting and production
Storage problems don't stay in the storage area. They spread into the rest of the shop.
On the floor, operators spend time looking for sheets, checking whether the stack really is 3 mm, and waiting for the forklift. Every minute of that is machine time you're paying for through your hourly rate, which is where inefficiency ends up whether you like it or not.
Forklifts near the laser are a risk of their own. Some small shops tilt the tines down against the edge of the bed and back away slowly so the sheet slides off. It works, but we've also heard horror stories, like the Tempus Tools customer whose operator drove the forklift into the machine's light guard within two weeks of the laser being installed. The replacement part took a week to arrive, and the laser sat idle. A vacuum lifter is really the only safe way to move a sheet. (For more on getting the most from the forklift you do have, see forklift theory.)
In the office, the effect shows up in quotes. If the estimator doesn't know whether the material is in stock, or the price book is out of date, the quote waits while someone checks. A clear, detailed quote that reaches the customer within two or three hours tells them the shop knows what it's doing. A quote that waits on a stock check doesn't. We cover the link between response time and win rate in why quote speed can matter more than price.
What to consider when choosing sheet metal racks
Before you buy, work through these:
- Sheet size. Standard cassettes for 4 x 2 m sheets are built slightly larger, around 4.2 x 2.2 m. Oversized work needs custom racking or custom cassettes.
- Material mix and weight. List your material types, grades and thickness range, and work out the total tonnage. Pallet racking beam loads will dictate where heavy plate can go. A steel weight calculator helps here.
- How material gets to the machine. Decide between forklift, crane, vacuum lifter or an automated feed before choosing the rack.
- Floor space and access. Count the space around the rack for forklifts to get in, turn and back out, as well as the rack footprint.
- The concrete slab. Fifteen tonnes in one rack is a serious point load. Check what your slab can carry before anything is bolted down.
- Certification. Racking is a certifiable piece of equipment that needs engineering certificates. Don't build your own. If something fails, the personal liability falls on the owner.
- Remnants. Plan where offcuts will go from the start.
- Growth. A cassette system can be extended and moves you closer to automated handling later.
Racking imported from China usually works out cheaper than local suppliers, even with freight. It arrives as a bolt-together kit with a lead time of around 90 days. There's usually room to negotiate on price, more so with overseas suppliers than local ones.
Plan storage from day one
The cheapest time to get racking right is when the shop is set up. A new laser needs more than floor space: gas reticulation, compressed air, enough power, possibly a nitrogen generator, and material storage. All of it should be costed into the original project. Racking that goes in on day one pays for itself fastest.
Changing later is painful. On top of the cost, you need somewhere to put every sheet in the shop while the old racking comes out, the new racking goes in, and the cassettes are reloaded. That upheaval is why so many shops put it off.
Sheet storage, material tracking and quoting accuracy
Physical racking is only half the job. A shop also needs to know what material it has, what it paid for it, and what it should charge.
Some basic disciplines make that much easier:
- Record heat numbers. Sheets arrive in batches, and a tonne of 3 mm usually shares one heat number. Enter each delivery into your inventory records with its heat number.
- Use first in, first out. When a new delivery arrives, take out the sheets already in the cassette, put the new ones on the bottom, and put the older ones back on top.
- Don't barcode individual full sheets. Lifting every sheet to apply a label is slow and risky, and the labour cost adds up fast. Knowing what you're using from its position in the rack is enough.
- Do label remnants, ideally with two labels each. That's where labelling is practical, and where it saves the most money.
On the pricing side, material is usually the biggest part of a laser cutting quote, so prices that are out of date cost money on every job (how material prices affect laser cutting jobs covers this). Tempus Tools' material management keeps material prices in one place, so a price update flows through to every new quote. Accepted quotes carry through to production documents, so the operator gets the material spec from the quote instead of a verbal description.
Practical tips for organising sheet metal storage
- Get everything off the floor. Nothing should lean against posts or sit on the ground.
- Separate material by type, grade and thickness, and label every bay or cassette.
- In pallet racking, put the heaviest plate in the lowest bays. In a cassette system you have more flexibility, but keep thin material high and thick material low. Pulling 6 mm sheets from a high cassette is fine. Pulling 25 mm plate from the same height isn't.
- Store only rectangular or square remnants. Trim L-shapes down, because they hang out of the rack and get hit. Operators then need to know where to find long strips like 3000 x 500 mm and where to find squares like 1500 x 1500 mm.
- Make sure the remnant the programmer allocated is the one that gets cut. Operators tend to grab one that looks about right. If it's 10 mm shorter, the job still cuts, but the bigger part that needed that remnant later has to come from a new sheet. The scrap that creates adds up.
- Stage tomorrow's material before you go home.
- Use a vacuum lifter to move sheets, and keep forklifts away from the laser.
- Review damaged and slow-moving stock regularly, so the dollars in your racks are in material you'll actually use.
Remnant barcoding systems are worth considering once the basics are working. They take discipline, but so does everything else in a job shop.
Get the material off the floor first
Good sheet metal racks protect material, give floor space back, and keep the laser cutting instead of waiting. For most small and mid-size shops, the best value is a rollout cassette system for new sheet, vertical racks for rectangular remnants, and a vacuum lifter to move material between them. Automated towers and storage systems pay off only for shops with the volume and shift pattern to keep them busy.
Tidy racking also makes quoting easier. When everyone knows what's in stock and the price book is current, quotes go out faster and with more confidence.
Frequently asked questions
What are sheet metal racks used for?
Sheet metal racks store flat sheet and plate in a fabrication shop so it stays flat, undamaged and easy to reach. Good racking protects material from forklift damage and rust, makes it quicker to load the laser, and frees up floor space.
What is the best way to store sheet metal?
For most small and mid-size job shops, store new sheet flat in rollout cassette racks, keep remnants in vertical racks, and move sheets with a vacuum lifter. Keep material off the floor, separate it by type and thickness, and rotate stock first in, first out.
Are vertical or horizontal sheet metal racks better?
They do different jobs. Horizontal racks, especially rollout cassettes, suit full sheets because the material stays flat and supported. Vertical racks suit remnants and offcuts, because you can see and flip through them quickly in a small footprint. Many shops use both.
How do fabrication shops prevent sheet metal damage in storage?
Keep sheets off the floor and away from forklift traffic, avoid timber pallets that rust the bottom sheet, store heavy plate low, and move sheets with a vacuum lifter instead of forklift tines. Trim remnants to rectangles so nothing hangs out of the rack.
How does sheet metal storage affect production speed?
Every material change costs cutting time. With poor storage, a change can take around 15 minutes. A laser running two shifts with 12 changes a day can lose three hours of production. Staging cassettes beside the machine for the day's work cuts most of that.
Why does material organisation matter for quoting?
Estimators need to know what material is on hand and what it costs. When stock records or the price book are out of date, quotes wait while someone checks, and slow quotes lose work. Accurate, current material data lets a shop quote quickly and with confidence.
See how Tempus Tools helps fabrication shops manage material pricing and quote faster, or book a demo.
Read blog
Articles
Sheet Metal Bending: A Practical Guide for Fabrication Shops
How sheet metal bending works, what affects bend quality, and why formed parts can destroy your margins when not quoted properly.
Sheet metal bending is how most fabrication shops turn flat laser-cut parts into brackets, channels, covers and enclosures. It's also where a lot of quoting goes wrong. The press stroke takes seconds, but setup, tooling and handling can take far longer, and a part that looks simple on a drawing may not be possible to bend on your press at all.
This guide covers how the sheet metal bending process works, the terms that matter, what affects bend quality, and how to quote bent parts so the price reflects the whole job and not just the cutting.
Why bending matters to a job shop
Shops offer bending for a simple reason: that's where much of the money is. A lot of laser cutting work arrives as cut-and-fold, and a shop that can't fold often doesn't get invited to quote the job at all.
It adds up. In one small single-laser shop we work with, folding brings in roughly $15,000 for every $80,000 of cutting, close to 20% on top of cutting revenue. With an efficient setup and a good press brake operator, bending can carry better margins than cutting. Priced badly, it quietly eats the profit from the laser.
What is sheet metal bending?
Sheet metal bending is the process of forming a flat sheet along a straight line into an angle, so it holds a new shape. Repeat it along several lines and a flat blank becomes an angle bracket, a U-channel, a box or a full enclosure.
Most bending in fabrication shops is done on a press brake, a machine that forces the sheet between a punch (the top tool) and a die (the bottom tool). Some shops also use folding machines or panel benders, which clamp the sheet and swing the flange up. In many countries, "folding" and "bending" are used almost interchangeably.
How the sheet metal bending process works
A typical formed part goes through these steps:
- The flat blank is cut, usually on a laser, from a flat pattern that allows for the material stretching in each bend.
- Bend lines, directions (up or down) and the bend sequence are worked out, either by the press brake programmer or in offline software.
- Tooling is selected and set up on the press: the punch and die to suit the material, thickness and inside radius.
- The operator positions the part against the backgauge stops and the press forms each bend in sequence.
- The operator checks the angle and dimensions, and adjusts for springback.
The press stroke is the quickest part of that list. As one shop owner put it: "The stroke time is nothing. It's setup and handling."
Common sheet metal bending methods
Air bending
Air bending is the most common method. The punch pushes the sheet into a V-shaped die without forcing it to the bottom, so the sheet touches the tooling at three points: the punch tip and the two die shoulders. The bend angle is set by how deep the punch goes, which means one set of tools can produce many angles. Because the sheet isn't fully pressed into the die, it springs back, and the operator has to compensate.
Bottoming
In bottoming, the punch presses the sheet down onto the die so it takes the die's angle. It needs more force than air bending, but gives more consistent angles and less springback.
Coining
Coining uses much higher force to press the sheet into the die, forcing the bend tighter than its natural radius. It's precise, with almost no springback, but it's hard on tooling and needs a lot of tonnage. It's much less common in general job shop work.
Hems and safety folds
A hem folds the edge of the sheet back on itself to give a safe, stiff edge. A safety fold (or open hem) leaves a small gap. Both are usually done in two stages: a sharp bend with an acute tool, then a flattening step.
Key terms in sheet metal bending
What affects bend quality?
Material and grain direction
Different materials bend very differently. Mild steel is forgiving. Stainless springs back more. Harder aluminium alloys and tempers, such as 5083, can crack if the bend runs the wrong way relative to the grain.
The grain that matters is the crystalline grain from rolling, not the surface finish, which catches people out. Grain direction has to be considered when the part is placed on the sheet for cutting, not when it reaches the press brake. By then it's too late. Designers are often unaware of it, so the shop needs to catch it at the quoting or nesting stage.
Thickness, bend length and tonnage
The force needed to bend a part rises with thickness and bend length. A press that handles a 1 m bend in 6 mm steel may not have the tonnage for the same bend at 3 m. Quoting a part your press can't form is one of the most common mistakes in bending.
Bend radius and tooling
The die opening and punch radius set the inside radius. Tighter radii need more force and are more likely to crack. Designs that use several different radii on one part need more tool changes.
Reach and clearance
Some parts can't be bent because of the tooling, not the force. The press needs enough throat depth to reach the bend. And as a part is bent up, already-formed flanges can collide with the punch or the machine. Deep boxes and return flanges often need special tooling, such as gooseneck punches.
Part design
Holes too close to a bend line distort. Flanges that are too short can drop into the die. Symmetrical parts are easier for operators to get the right way round. Our tips for folding and bending laser cut parts cover the main design rules.
The flat pattern
If the K-factor or bend deduction is wrong, the flat blank is cut to the wrong size and the finished part comes out short or long. That's a common problem when the flat pattern produced at quoting is reused for production. For anything other than mild steel, check the unfold uses the right values for that material and thickness. For a cover on a ute, a millimetre won't matter. For a precision part, it will.
Why bending matters when quoting sheet metal parts
Quoting a bent part means answering two questions. What will it cost? And can we actually make it?
What it costs: setup plus handling
The price of bending splits into setup time and bending time.
Setup starts with getting the right punches and dies from the rack. Then it often means setting up several stations along the press. On a 3 m press brake, a part may need three or four setups to complete. Take a 500 x 300 mm tray with flanges on all four sides. The 500 mm sides need a 500 mm tool, but once they're bent, a 500 mm tool would crush them when you turn the part round for the 300 mm sides. So you need a 500 mm station and a 300 mm station. Parts with folds inside other folds can need more.
Some setups add further steps. A bend at an angle to the edge of the part needs a guide on the bed so the part can be positioned correctly. A split fold (where the two ends are bent but the middle isn't) needs an extra stop to locate the part sideways.
Bending time is mostly handling, not pressing. One customer told us a story about a part they quoted with Tempus Tools that was almost 3 m long in 1.6 mm brushed stainless. "It's like trying to fold a piece of tissue paper," was how it was described. It couldn't be scratched, so it couldn't be dragged across tables. It needed three people to lift, a protective film on the tooling, and a full flip part-way through because some bends went the other way. That flip was the most expensive move in the whole job.
Large parts also slow things down at the backgauge. With three or four stops across a long part, you often need a second person to check it's hard up against every stop before the operator presses the pedal.
Can you make it?
The harder question is feasibility. Before quoting a formed part, a shop needs to know:
- Does the press have enough tonnage for this thickness and bend length, without damaging the tooling?
- Does it have the reach (throat depth) and tooling to get to each bend?
- Can each bend be reached without the part hitting the tooling, given the design?
- Are there manufacturability issues, like holes too close to bends?
Without a simulation, many shops add up the bends, allow 10% extra and hope. The risk is quoting a part that can't be folded at all.
In smaller shops, the usual answer is to walk out and ask the press brake operator. That interrupts production. If the operator has to simulate the part on the press controller, that can cost 30 minutes of machine time for one quote. Experienced operators can often look at a drawing and tell you it won't work, but that's not a reliable basis for quoting either. (We've written before about keeping your press brake operator out of quoting.)
Shops with offline press brake programming software can run a simulation on complex parts before they quote. That confirms the part can be bent and gives realistic bend times to price from.
Common quoting mistakes with bent parts
- Pricing only the cutting and treating a formed part like a flat one
- Assuming one setup covers every bend
- Forgetting the handling time for large, thin or cosmetic parts, including extra people, flips and protective film
- Quoting a bend length and thickness the press doesn't have the tonnage for
- Missing collisions and reach problems that make the part impossible to form
- Leaving out other secondary processes on the same part, like welding, countersinking or powder coating
- Pulling the press brake operator off the machine to estimate every job
How shops can price bending more consistently
Most of the cost of bending is predictable if you have rules for it. Part size, weight and the number of bends drive setup and handling time, and those can be priced the same way every time instead of from memory.
A practical example is a handling allowance based on area: once a part exceeds a set size, say 4 square metres, the rule adds time for a second or third person. Heavier parts, cosmetic finishes that can't be scratched, and parts needing a flip can carry similar allowances.
Tempus Tools lets shops set up secondary process pricing for folding, welding, powder coating and other steps, priced from each part's properties, so bending lands on the same quote as the cutting instead of being added by hand. For customers who send 3D models, the 3D sheet metal extractor unfolds STEP and IGES files into flat parts ready to quote. See how it fits together for sheet metal shops.
Rules won't answer the feasibility question on complex parts. That still needs an experienced eye or a simulation. But they take the guesswork out of routine bent parts, and they stop the estimator walking out to the press brake for every quote.
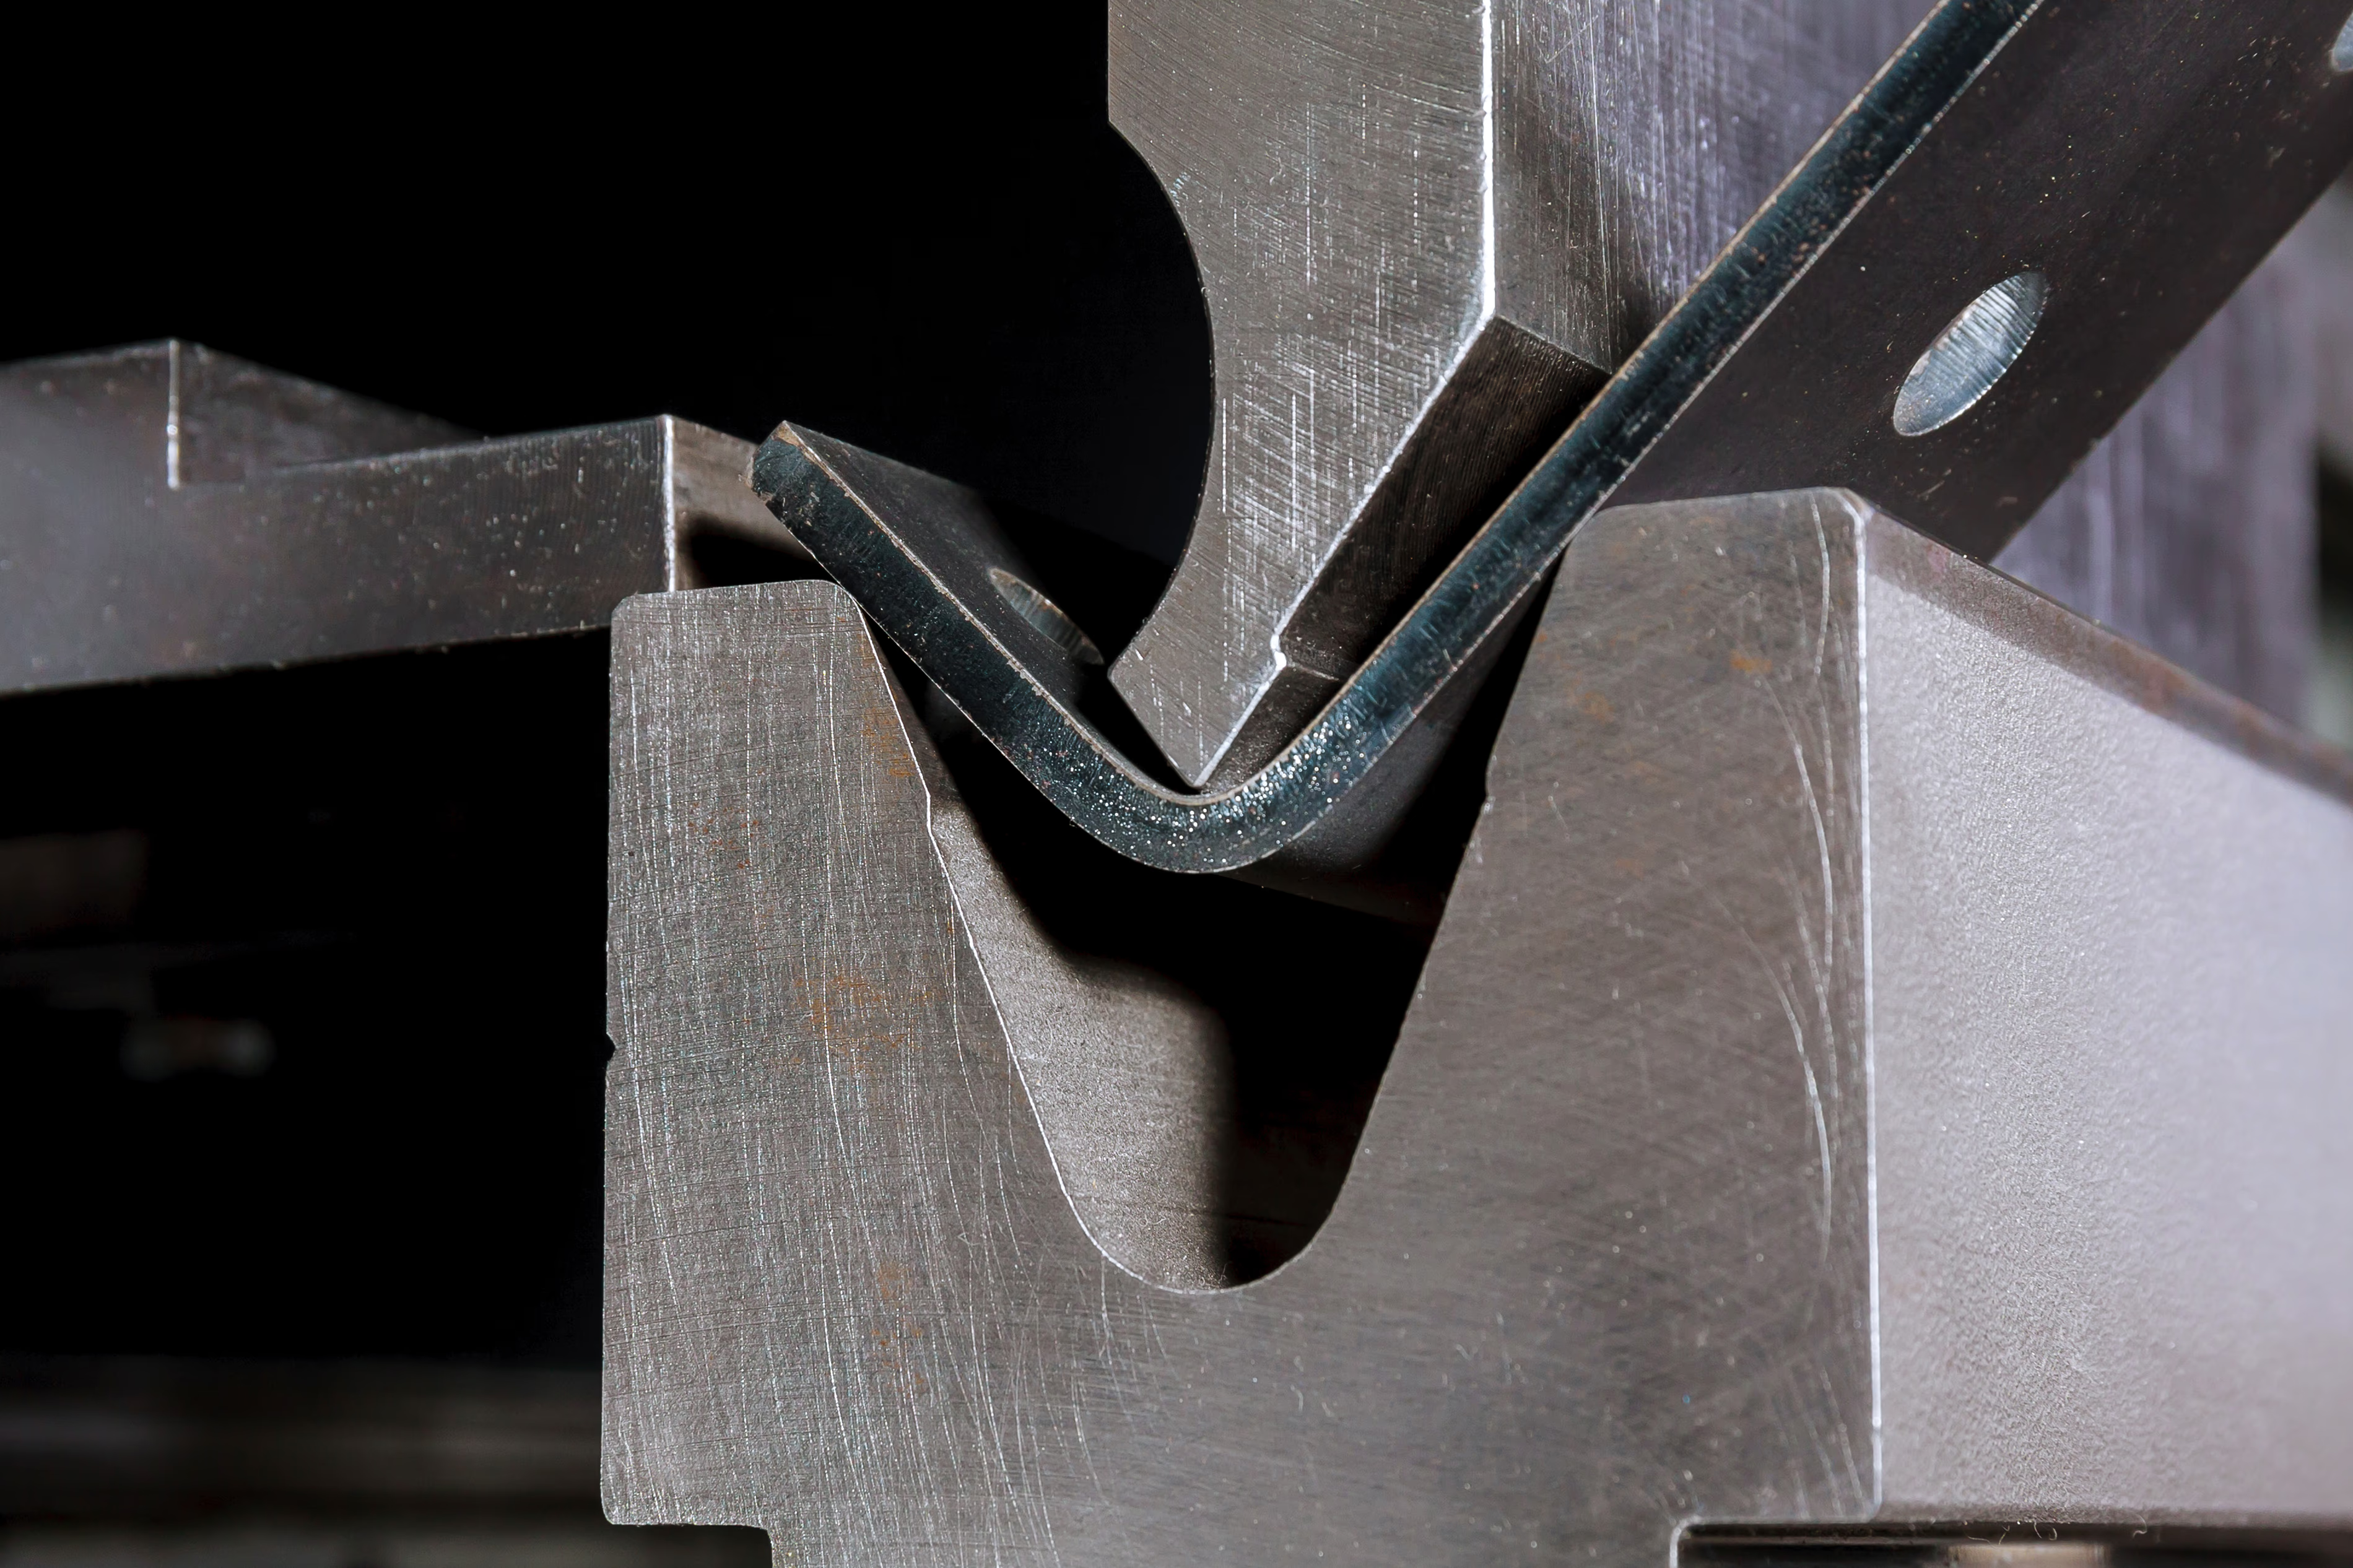
Sheet metal bending and the production handoff
Once a quote is accepted, the information that went into it needs to reach the floor. For bent parts, that means:
- The correct flat pattern for cutting, unfolded with the right K-factor for the material
- The part's orientation on the sheet if grain direction matters
- Bend directions, sequence and any notes on special tooling or handling
- Part labels so operators can match cut blanks to the right job
- Work orders that show which parts need folding and which go straight to dispatch
When that information is missing, the operator works it out again from the drawing, which repeats work done at quoting and invites mistakes. Production documents generated from the quote carry the job details through, so the floor works from the same information the price was based on.
Price the whole formed part
Sheet metal bending is one of the most valuable services a job shop can offer, and one of the easiest to underprice. The press stroke is quick. Setup, tooling, handling and the question of whether the part can be bent at all are where the time and risk sit.
Quote formed parts on the full workflow: cutting, setup, handling and every other process the part needs. Use rules for the routine work, and save the operator's time and the simulation for the parts that need it.
Frequently asked questions
What is sheet metal bending?
Sheet metal bending is the process of forming flat sheet along a straight line into an angle, using force from a press brake or folding machine. Several bends turn a flat blank into brackets, channels, trays and enclosures.
What machine is used for sheet metal bending?
Most shops use a press brake, which forms the sheet between a top punch and a bottom die. Folding machines and panel benders are also common, particularly for long, thin sheet. The machine's tonnage, bed length and throat depth decide which parts it can bend.
What is bend radius in sheet metal?
Bend radius is the radius of the curve formed at a bend, usually measured on the inside. In air bending it's set mostly by the die opening. As a starting rule, keep the inside radius at least equal to the material thickness to avoid cracking.
What is bend allowance?
Bend allowance is the length of material that goes into a bend, measured along the neutral axis. It's added to the flange lengths to calculate the flat blank size, and it depends on the material, thickness, bend radius and K-factor.
Why does bending affect the price of a sheet metal part?
Bending adds setup, tooling changes, operator time and handling, and large or cosmetic parts may need extra people. The press stroke itself is quick, so the cost depends on how many setups the part needs and how hard it is to handle.
How do fabrication shops quote bent parts?
Good quotes check feasibility first (tonnage, reach and tooling), then price setup and handling alongside the cutting. Many shops use pricing rules based on part size, weight and bend count, and run complex parts through bending simulation software before committing to a price.
See how Tempus Tools helps fabrication shops price cutting, bending and secondary processes together, or book a demo.
Read blog


ROI Calculator
See how much time and money you’ll save
Use our ROI Calculator to measure potential labor savings, faster quoting, and increased consistency for your shop.
Resources
Success stories
Success stories
0
min read
US job shop Hammers home success with attitude-first hiring
Facing skilled labor shortages, Hammer MetalWerks shifted its hiring strategy to prioritize attitude over experience, using technology to quickly train new operators. With Tempus Tools streamlining quoting, work orders, and secondary processes, the team has improved accuracy, reduced errors, and empowered new staff to become productive faster.
A US-based metal fabrication job shop is taking a new approach to hiring staff, in response to skilled labor shortages, preferencing work ethic and attitude over existing skillset.
Derek Hammer, President of Hammer MetalWerks, and Erin Hammer, Vice President and Director of Human Resources have found that with the right technology, you can train and upskill an employee with a good attitude, which benefits them and the business.
“Our laser operator and brake press operator had both never used those machines in their life before working here. But they were intelligent, familiar with computer systems, and had a positive attitude to learning, so we hired them based on that,” said Derek.
Hammer MetalWerks provides small-to-medium production runs and parts for a huge range of industries, from construction, to healthcare, entertainment, attractions, military, and government.
“Rather than looking for highly skilled – and more expensive – operators, which are in short supply, we looked for technology that could make the operator’s job easier, and help them get up to speed faster,” says Derek.
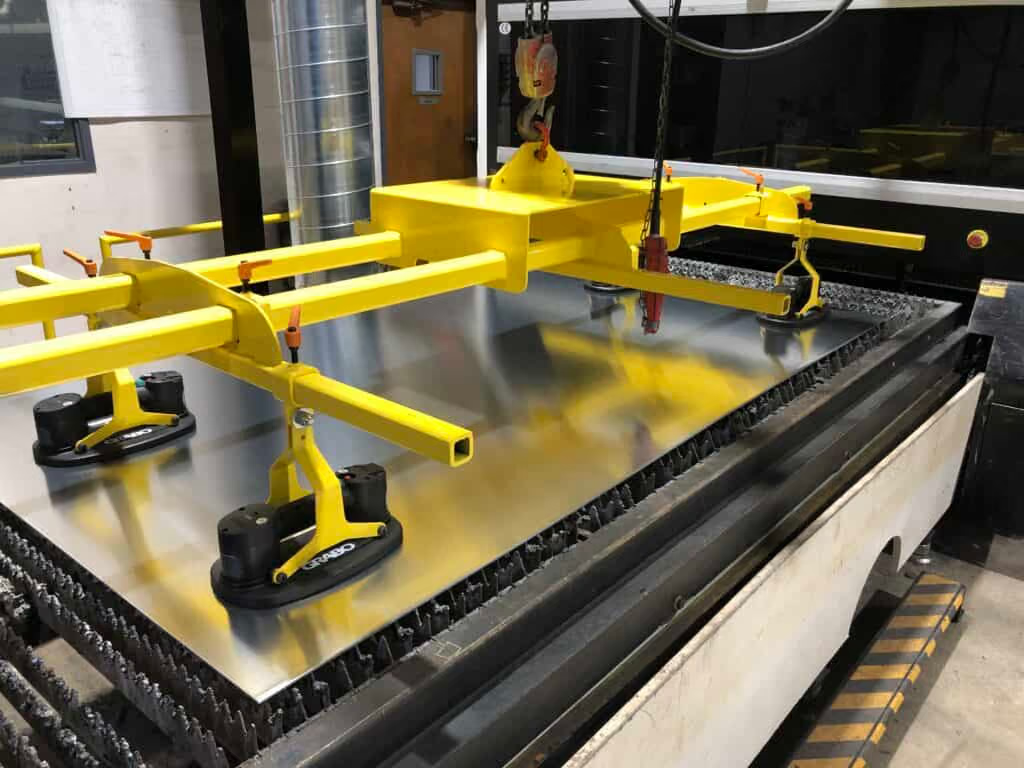
Hammer chooses Tempus Tools
One technology the Hammers chose to help their new staff, and the overall efficiency of the job shop, was Tempus Tools. Tempus Tools is multi-functional laser cutting quoting software that is calculation-based and runs on a Software as a Service (SaaS) model. It can be set up with information on material price, cutting time, labour, and other relevant information, to generate quotes quickly and accurately.
“Tempus Tools has been highly valuable for us. It provides work orders to the shop floor with lots of details that the operators don’t have to find or calculate themselves. One example for us is that sheet sizes are all metric, and we use imperial gauges in the US – which can often lead to errors if not converted correctly,” explains Derek, whose business operates a 3kW fiber laser machine.
“Moreover, 11 gauge aluminium is not the same thickness as 11 gauge steel, and our laser machines are all metric, so having all the right measurements through Tempus Tools reduces the risk of any errors.”
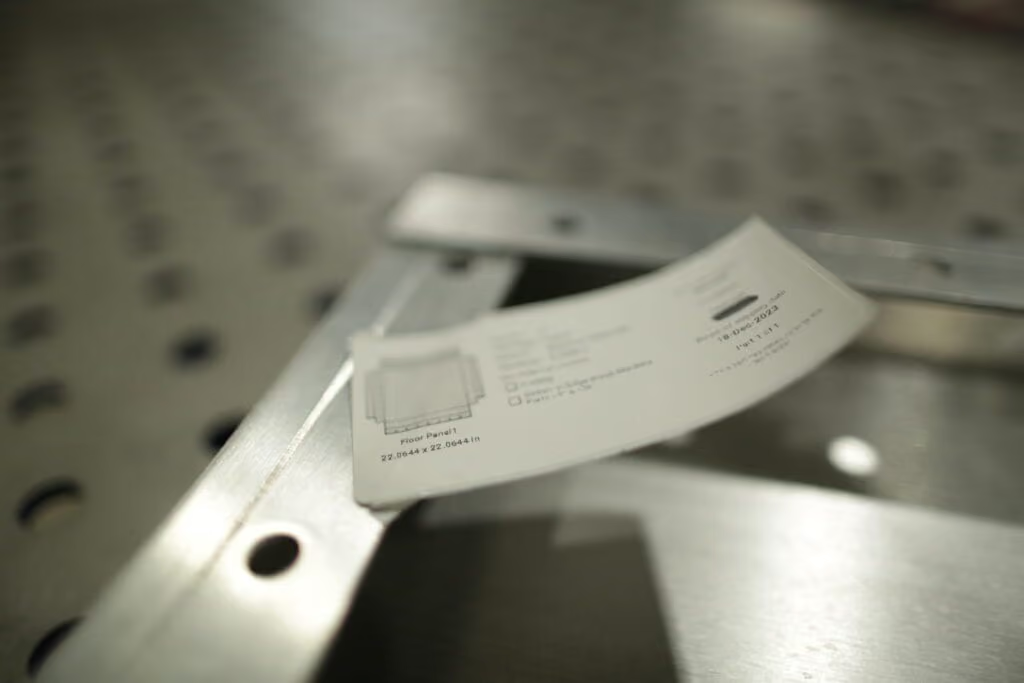
“Additionally, Tempus Tools is very user-friendly, so staff that are used to working with computers in a broad range of contexts can pick up the program quickly and begin working with it.”
Tempus Tools CEO, Bart Jesman, says it’s rewarding to see the software benefitting forward-thinking job shops like Hammer MetalWerks. “We’ve designed Tempus Tools to provide benefits to job shops of all shapes and sizes. What Derek has done is take this a step further and used it to improve his hiring process, by making the operator’s job easier – it’s an intelligent approach.”
Secondary processes
In addition to metal fabrication and laser cutting, Hammer MetalWerks has a unique advantage over most job shops, with the broad range of additional services and secondary processes it provides, including design, bending, welding, powder coating, packaging, tapping, rivets, hardware, and more, all from the one place.
“With so many secondary processes, it’s so helpful that we can quote them all using Tempus Tools, and they can all be included in the work order that goes out to the shop floor,” says Derek.
“Additionally, the work order can be sent to our label printer, including a thumbnail of each item, to provide a visual cue to our shop floor staff, to further enhance the accuracy and efficiency of their work. It really helps avoid mix-ups on the shop floor.”
Updates and support
Derek adds that the support from the Tempus Tools team has been outstanding, collaborative, and helpful.
“The Tempus Tools team is always open to feedback, and they use this to help develop new features that make Tempus Tools better for job shops like ours. But they’ll also help with general questions we have – and they have experienced staff to draw upon for industry knowledge,” he says.
“With the skilled labor shortages in the US – and common issues around the world – having the right technology is crucial. We now hire employees that fit well with our work culture and have a good attitude – and it’s working out well for our business,” concludes Derek.
To learn more about Tempus Tools, please click here.
Read blog
Success stories
0
min read
From quoting crunches to streamlined processes: Tempus Tools empowers growth of J&T Steel Sales
As J&T Steel Sales expanded into the fast-growing laser cutting market, outdated spreadsheet-based quoting quickly became a bottleneck for delivering fast, reliable service. By adopting Tempus Tools, the team streamlined quoting, order tracking, and invoicing—freeing up time, improving consistency, and supporting the company’s growth as they scale their laser cutting operations.
Expanding Australian metal fabrication specialist, J&T Steel Sales, has found that improved productivity and new equipment is only half the battle to boost customer service and sales – equally important is eliminating the outdated processes used to track and prepare quotes, delivery, and invoices.
J&T Steel Sales began as a small plate processing business in Victoria with a CNC Plasma machine, where staff used spreadsheets to develop quotes for customers, but the company has now made the move into the high demand laser cutting market.
Part of the motivation for the expansion was a need in the market for better lead times on laser cut metal products, including aluminium, stainless steel, and carbon steel.
“We had customers come and beg us to purchase a laser machine, because they were fed up with the long lead times that were becoming increasingly common for laser cut products,” explains Luke Patterson, Operations Manager, J&T Steel Sales.
“So we invested in a laser cutting machine, and prepared to grow our business to the next level. But with this change, we needed a quick and efficient software solution to export a presentable quote that we can forward directly to customers in a timely fashion. Spreadsheets just weren’t going to work anymore, so we did some research and found Tempus Tools,” he said.
Laser cutting quoting software streamlines operationsTempus Tools, is a multi-functional laser cutting quoting software that is provided using a SaaS (Software as a Service) model. Tempus Tools was developed specifically for the laser cutting industry, and is designed to save job shops time, and make quoting more efficient, accurate, and consistent.
“Tempus Tools has allowed us to streamline not only the quoting aspect, but also the tracking of active orders as well as invoicing,” says Luke.
“It has been able to take most of the heavy lifting in cutting back on excess paper waste in our offices, whilst also creating a digital paper trail to be able to track material usage and stock.”
Since purchasing the laser cutting machine, J&T Steel Sales has committed to getting customers their parts when they need them, calling it “the J&T Guarantee”.
“Tempus Tools has helped us immensely in delivering this guarantee to our customers. It has taken the stresses and late night quoting crunches and completely streamlined the process, freeing up more time for us to be able to focus on growing the business,” says Luke.
“In the past, expanding our customer base meant we would fall increasingly behind when it came to invoicing and quoting. Now, with Tempus Tools, we really feel we have found a software that not only services us now, but also allows us room to grow in the future.”
Service is key
Luke explains that in his business, customer service is the key to success. Customers have good memories, and they value pricing consistency, accuracy, and reliability.
“Being a service-focused business, it’s something I look for in our suppliers too. In my opinion, the Tempus Tools team has been exceptional when it comes to responsiveness and availability to work through any challenges I’m experiencing,” he says.
“Coming from a small business ourselves it was an incredibly refreshing experience to have team members visit our workshop, and to also feel listened to when it came to our concerns or feedback for the future development of Tempus Tools.”
“I met Mark Washington (Sales & Support) and Felipe Lechuga (Director) from Tempus Tools at a local manufacturing expo earlier this year, and they took the time to visit our job shop and discuss the functionality of Tempus Tools, and what more it could be doing for us. I was very impressed, and I’m grateful for all the support.”
A bright future
J&T Steel Sales has seen steady growth since moving into the laser cutting business, and Luke has plans to continue this trend.
“Our future plans are not only to focus on bringing in new customers – ideally ones that require repeat work – but also to let all our customers know about our bending and fabrication facility, so they know we can provide an end-to-end manufacturing solution,” he says.
“Tempus Tools has a huge range of useful features, and the development team is always working on new functionality that can benefit job shops like ours, so it is a key component of our growth plans.”
To learn more about Tempus Tools, please click here.
Read blog
Success stories
0
min read
MSG Industries provides laser cutting quotes eight times faster with game-changing software
After struggling with an in-house quoting system that was costly and inefficient, MSG Industries adopted Tempus Tools and immediately cut quoting time while improving accuracy and pricing consistency. The team now relies on Tempus Tools powerful features—like PDF part extraction and upcoming pipe-cutting support—to streamline operations and better serve their growing customer base.
A Canadian metalworking, fabrication, welding, and laser cutting enterprise, MSG Industries, has implemented a “game-changing software” to deliver faster and more accurate laser cutting quotes to its customers.
MSG Industries Vice-President, Olivier Samson, had been working with his team on developing their own quoting tool software, but it was not a cost-effective solution to the accuracy and time pressures the growing business was facing.
“We probably spent about $15,000 (Canadian dollars) and a large investment of hours developing a home-made system, but it just wasn’t performing to the level we needed to deliver better service to our customers,” said Samson.
“We did some research and discovered Tempus Tools, and it’s a game-changing software for us. Right now, I can’t imagine how we could get through the week without it,” he added.
MSG Industries, which prides itself on innovation, integrity, and professionalism, has been growing steadily since its inception three years ago, and to cope with additional requests for quotes, the company took on two full-time employees dedicated to quoting.
Tempus Tools, is an all-in-one laser cutting quoting software that is provided using a SaaS (Software as a Service) model.
“Since implementing Tempus Tools, we’ve found it is much more accurate, reliable, and fast. Instead of two people quoting full time, we can now have one person do a better job in a quarter of the time, freeing up staff to work on other tasks that can further grow our business,” says Samson.
“As we take on more customers, and send out more quotes, Tempus Tools also gives us total pricing consistency, which means we build the trust of our customers. No one likes receiving two different prices for the same work, but if two different estimators manually prepare the quote, it can happen,” he says.
“Additionally, the service has been outstanding, which is rare these days. Every time I’ve needed assistance, the Tempus Tools team has been quick to respond and highly professional.”
New updates: pipe cutting
MSG Industries provides services to a broad range of industry, and is constantly looking at ways to innovate and expand its offering.
“Our strength has always been our versatility. We have a department dedicated to heavy structural fabrication, such as schools or hospital building pieces, another department for food factory equipment, one for hydropower products, and then we have pipe cutting and laser cutting services,” explains Samson.
“Since we have so many different departments, we need very reliable tools to help us quote, and Tempus Tools has been highly valuable to us.”
“Our major focus right now is working on our pipe cutting laser service, and Tempus Tools is already working on adding this functionality into Tempus Tools so that we can quote for this service too – it’s very exciting.”
Turning customer PDFs into quote-ready CAD files
Tempus Tools Director Felipe Lechuga says that the discovery of Tempus Tools PDF part extractor feature was a further benefit to MSG Industries.
“MSG had just been using Tempus Tools for creating new quotes, but when they discovered they could use the PDF part extractor to turn a customer’s vector PDF into a CAD file straight away with no tracing required – they were delighted with the results,” said Lechuga.
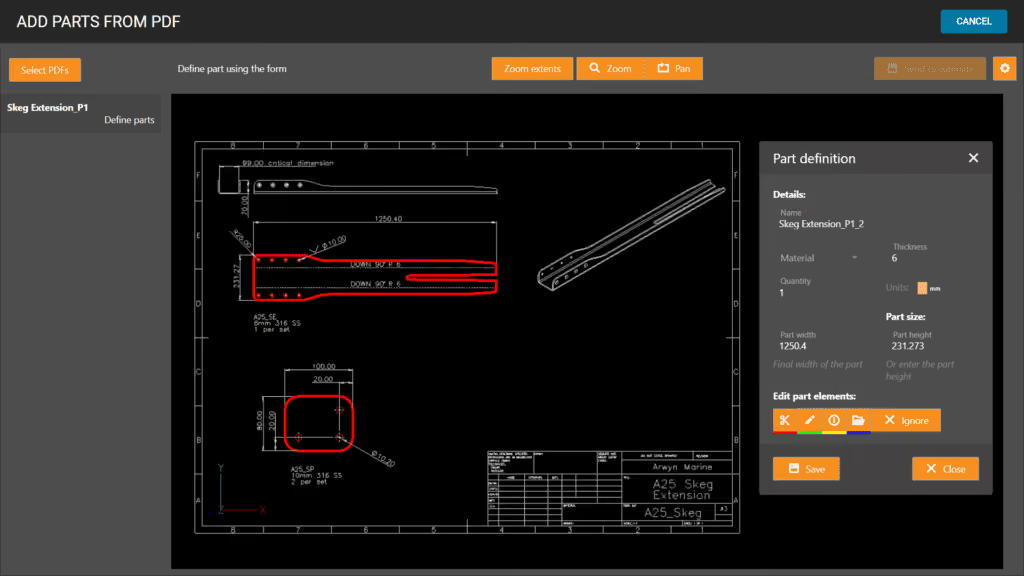
“The PDF part extractor doesn’t need any CAD package or skills to use, meaning anyone can simply click on a part and extract it into a quote. You can scale the part, plus specify details like folding and etching too.”
Olivier Samson says he can’t believe he didn’t try the PDF part extractor right away. “This is even more than we hoped for. Such a useful tool! I wish we’d tried out these features from the beginning.”
“I’ve found that Tempus Tools is reliable and fast, and Tempus Tools is actively working on updates, so we really couldn’t ask for more!” he concluded.
Read blog
Resources
Product updates
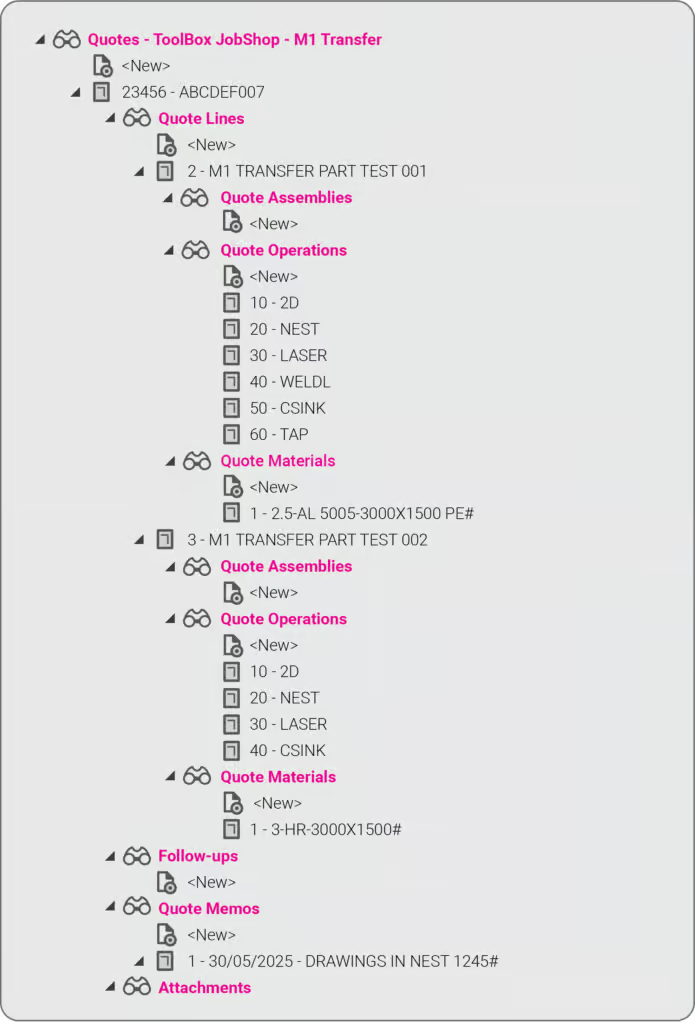
Product updates
0
min read
New integration: Tempus Tools + ECI M1 – from quote to order to ERP, seamlessly
At Tempus Tools, we know that speed and accuracy are everything in a laser cutting job shop, and today we’re announcing a new integration that makes both even easier.
We’re now fully integrated with ECI Software’s M1 ERP system.
What does that mean for your job shop?
It means you can now send quotes, order details, and production-ready drawings directly from Tempus Tools into your M1 ERP — no more double handling, no more data entry errors, no more jumping between systems.
This integration eliminates any “dead zone” between quoting and production. You get the specialist laser quoting power of Tempus Tools (like lightning-fast nesting, material cost accuracy, and margin control) combined with the operational backbone of M1.
It’s quoting that talks to your shop floor.
We’ve talked about how integrations like Google Drive can supercharge job shop workflows, and this M1 integration is another great example.
Want to learn more or set it up? If you want to avoid the limitations in the generic quoting functions in ERP/MRP software, but still use the rich planning and production features in ERP/MRP software, then get in touch today.
Book a demo or email us at support@tempustools.com and we’ll help you get connected.
Tempus Tools + M1 = quoting to production, finally in sync.
Read blog
Product updates
0
min read
Tempus Tools’ Google Drive integration: 6 ways to supercharge your job shop efficiency
Tempus Tools’ new Google Drive integration automatically saves your quote data and part files to Drive, opening the door to faster, smarter workflows. In this post, we highlight six clever ways job shops are already using it to boost efficiency.
Last month Tempus Tools released a powerful new feature: seamless integration with Google Drive.
Since then, we’ve heard from lots of customers about the innovative ways they have implemented this integration in their job shops, and we wanted to share the best six with you to inspire you to use the feature in your shop.
First, a quick recap: with the Google Drive integration, all your quote data (in CSV format) and production-ready part files can be automatically saved to your chosen Google Drive folder. From here, they can be exported to any number of programs or that data can be manipulated for many use cases, opening up a world of automation, reporting and connectivity for your job shop. We’ve also put together a quick video to show the integration in action.
1. Automate quote data collection for reporting
With every quote automatically saved, you can easily compile and analyse your quote performance over time. Use Google Sheets or your favourite analytics tool to track:
- win/loss rates
- performance across material types
- average order size
- breakdown of secondary processes contributions
This data-driven approach helps you identify trends, optimise pricing and improve customer response times.
2. Connect with ERP/MRP and other business systems
Some apps have native integration with Google Drive, which makes taking in quote data and parts easy, but many need a formal API. Luckily, Google Drive comes with its own API.
Some users have used the Google Drive API to build automations that push quote data directly into ERP, MRP or order management systems. This can streamline order processing, reduce manual data entry and ensure your production schedule is always up to date.
3. Organise your orders by material type
Use the exported quote data to create a parts planner that groups jobs by common material type. This enables you to:
- batch similar jobs for more efficient material usage
- reduce changeover times on machines
- optimise purchasing and inventory management
A simple Google Sheets script or integration with a dashboard tool can make this process nearly automatic.
4. Integrate with project management tools
Connect your quote data with popular tools like ClickUp, Monday.com or Airtable. Build custom dashboards and planners for your factory, visualise job statuses and assign tasks to your team-all based on real-time quoting data. These tools don’t require coding or a developer and anyone can work wonders. These types of projects boost collaboration on the shop floor and keep everyone aligned on priorities.
5. Create a scheduling calendar from time calculations
Use the time estimates in your quote data to automatically populate a production calendar. With a Google Calendar integration, you can:
- visualise machine and operator workloads
- identify bottlenecks before they happen
- easily adjust schedules as new jobs come in
This proactive scheduling helps you deliver on time, every time.
6. Enable automated notifications and workflows
Set up Google Drive triggers (using tools like Zapier or Google Apps Script) to notify your team when new quotes are confirmed as orders, or to kick off downstream processes-like updating CRM records or ordering materials.
Getting started is easy
- Go to Settings > Organisation settings > Integrations in your Tempus Tools Tempus Tools account
- Connect your Google Drive and select your preferred folder
- Choose the quote statuses that will trigger automatic file saving
- Start building automations and workflows that fit your shop’s needs
This integration is designed to be flexible-whether you want to automate reporting, connect with business systems, or simply keep your files organised, Tempus Tools and Google Drive make it possible.
Ready to enhance your job shop efficiency? Try the new Google Drive integration today.
Read blog
Product updates
0
min read
Tempus Tool’s new laser cutting quoting experience
Tempus Tool's new quoting interface delivers faster calculations, cleaner navigation, and powerful new features—all in one unified, intuitive screen. From smarter sorting to automatic updates and richer quote details, the upgraded experience makes quoting simpler, quicker, and more efficient than ever.
After months of rigorous development and innovation, we’re thrilled to unveil the newest evolution of our quoting interface in Tempus Tools. We remain committed to enhancing your laser cutting quoting process. This fresh approach promises enhanced navigation, lightning-fast calculations, and a host of exciting new features.
We have collected your feedback and listened to your concerns and requests over the past couple of years, and our design team has used their magic to put together a quoting interface that takes Tempus Tools to the next level!
Watch our new Tempus Tools Overview video to see all changes in detail:
Read on to learn more about some of the enhancements.
Tailored sorting
You’re in complete control. Choose between the smart auto-sort feature or manually arrange parts using drag-and-drop for a seamless organisation that aligns with your preferences.
Material requirements and order summary
At a glance, get an indication of how many sheets you need of each material to fulfil the order. Additionally, the order summary details information such as the total order weight, processing time and part count.
Part notes for everyone
A dedicated section for notes, whether they come from your customers, your team, or personal reminders for a job.
Streamlined price adjustments
With our revamped interface, tweaking the prices of parts becomes an intuitive and quick task.
Extra quote details
From setting an RFQ number to determining invoice due dates, shipping options, and beyond – we’ve got it all.
Unified quoting screen
No more toggling between tabs. Every bit of information you need, all consolidated on a single, intuitive page.
Automatic calculations
Forget the constant back and forth with the Calculate and Edit buttons. Our system now recalculates on-the-fly, keeping up with your pace.
Sleeker interface
With a cleaner, fresher look, onboard new team members with ease and navigate your daily tasks faster.
Customer emailing enhancements
An integrated system to keep your customers in the loop for every quote status.
In short, quoting in Tempus Tools is now even simpler and smarter. We’ve made sure it’s user-friendly while still being packed with all the features you need. Dive in and check out all the new improvements!
Accessing the new quoting experience
If you’re new to Tempus Tools, you will get the new experience by default. Just create a Tempus Tools account to get started.
For existing users, you have a temporary period to switch back and forth between the old and new experiences using the toggle at the top of the quote page.
We believe the new quoting experience will significantly enhance your quoting efficiency, and we can’t wait for your feedback.
Read blog
Ready to take a closer look at Tempus Tools?
Find out if Tempus Tools is a good fit for your shop in just 30 minutes.
Upload your own parts for a live demo
Get answers to pricing and setup questions
No-pressure call focused on your workflow