
Sheet Metal Bending: A Practical Guide for Fabrication Shops

05 Oct 2026
Sheet metal bending is how most fabrication shops turn flat laser-cut parts into brackets, channels, covers and enclosures. It's also where a lot of quoting goes wrong. The press stroke takes seconds, but setup, tooling and handling can take far longer, and a part that looks simple on a drawing may not be possible to bend on your press at all.
This guide covers how the sheet metal bending process works, the terms that matter, what affects bend quality, and how to quote bent parts so the price reflects the whole job and not just the cutting.
Why bending matters to a job shop
Shops offer bending for a simple reason: that's where much of the money is. A lot of laser cutting work arrives as cut-and-fold, and a shop that can't fold often doesn't get invited to quote the job at all.
It adds up. In one small single-laser shop we work with, folding brings in roughly $15,000 for every $80,000 of cutting, close to 20% on top of cutting revenue. With an efficient setup and a good press brake operator, bending can carry better margins than cutting. Priced badly, it quietly eats the profit from the laser.
What is sheet metal bending?
Sheet metal bending is the process of forming a flat sheet along a straight line into an angle, so it holds a new shape. Repeat it along several lines and a flat blank becomes an angle bracket, a U-channel, a box or a full enclosure.
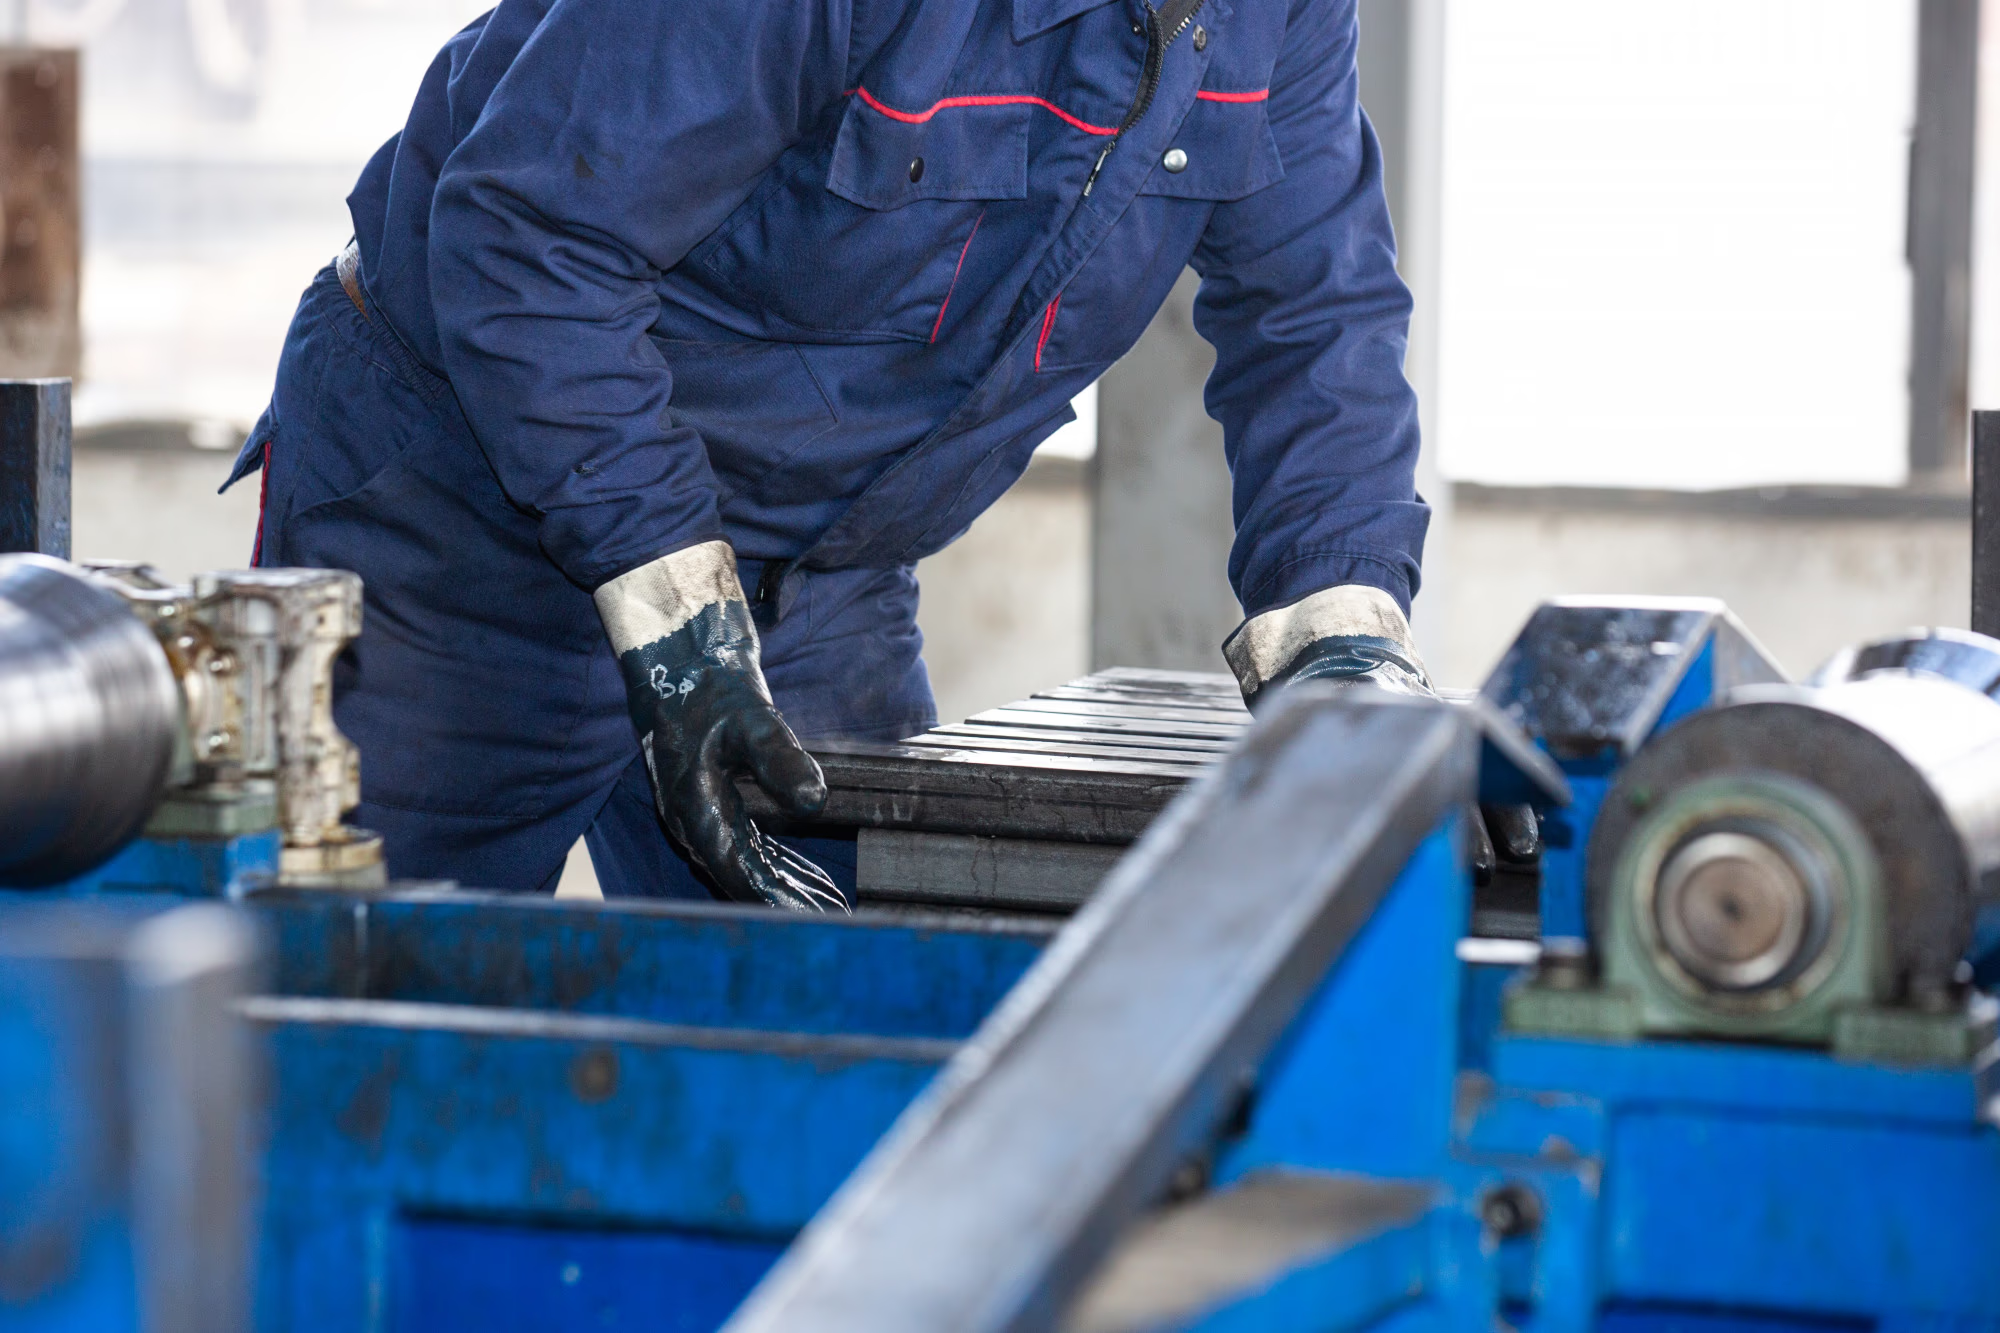
Most bending in fabrication shops is done on a press brake, a machine that forces the sheet between a punch (the top tool) and a die (the bottom tool). Some shops also use folding machines or panel benders, which clamp the sheet and swing the flange up. In many countries, "folding" and "bending" are used almost interchangeably.
How the sheet metal bending process works
A typical formed part goes through these steps:
- The flat blank is cut, usually on a laser, from a flat pattern that allows for the material stretching in each bend.
- Bend lines, directions (up or down) and the bend sequence are worked out, either by the press brake programmer or in offline software.
- Tooling is selected and set up on the press: the punch and die to suit the material, thickness and inside radius.
- The operator positions the part against the backgauge stops and the press forms each bend in sequence.
- The operator checks the angle and dimensions, and adjusts for springback.
The press stroke is the quickest part of that list. As one shop owner put it: "The stroke time is nothing. It's setup and handling."
Common sheet metal bending methods
Air bending
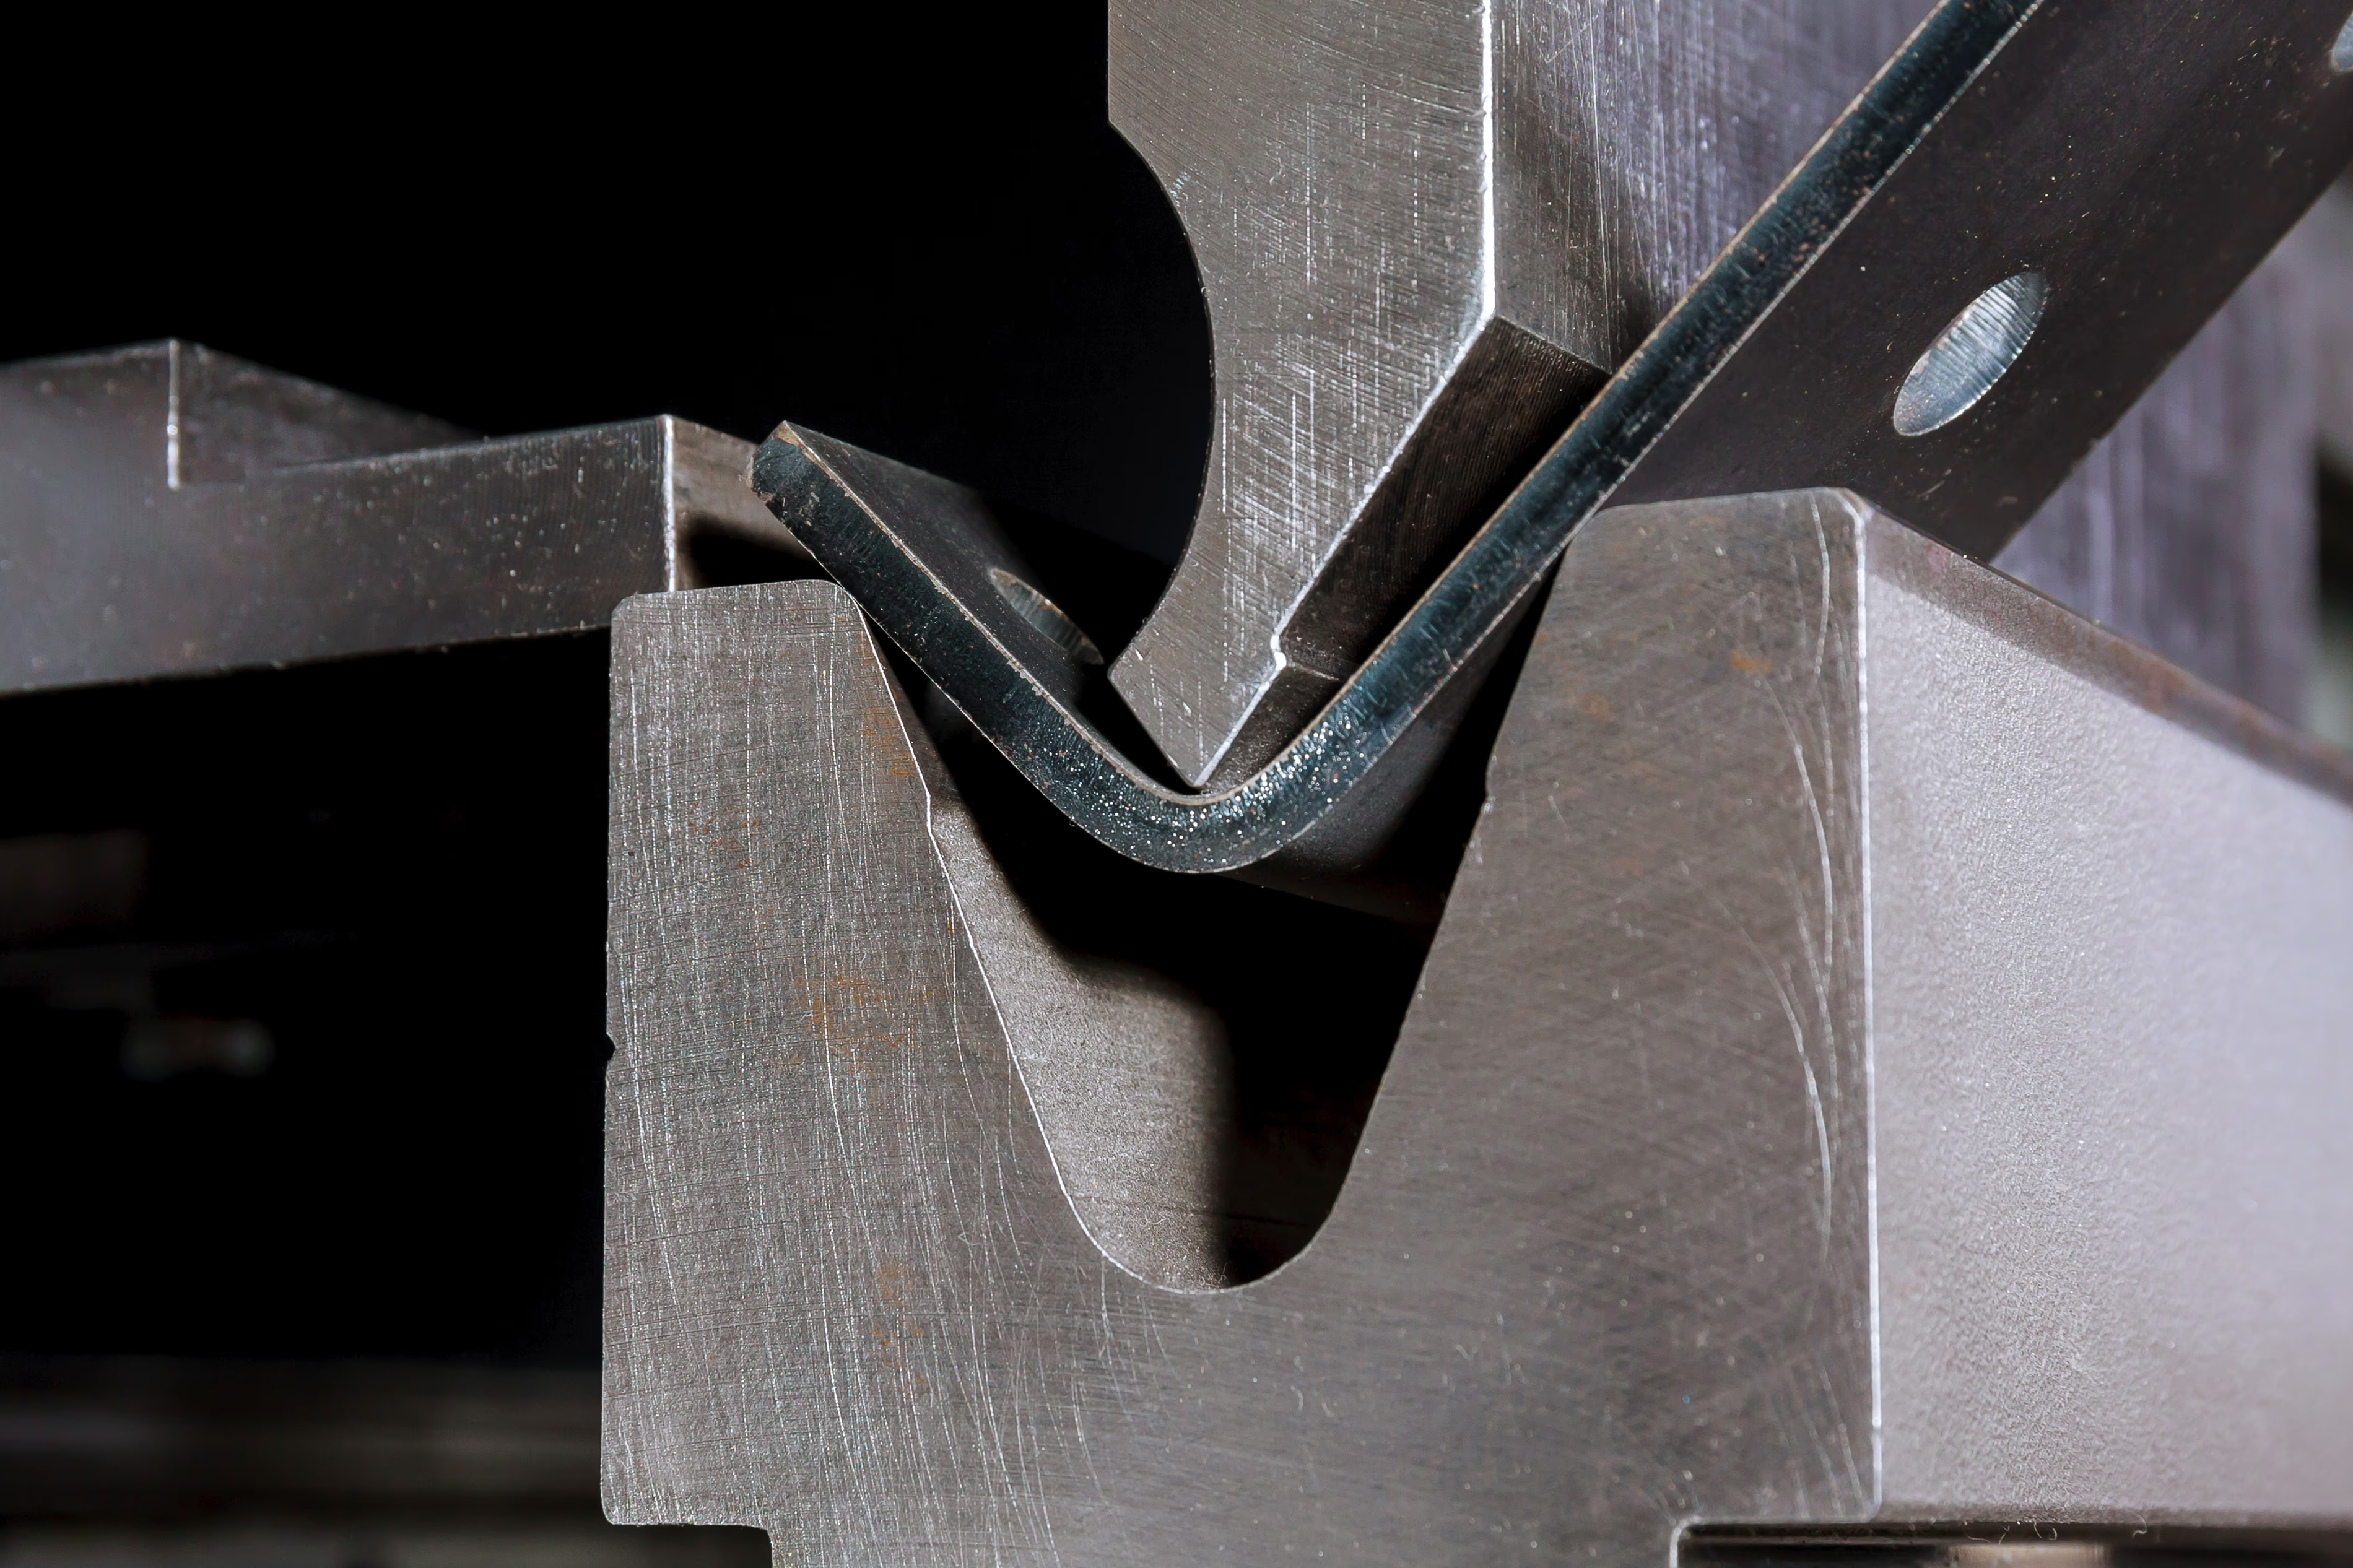
Air bending is the most common method. The punch pushes the sheet into a V-shaped die without forcing it to the bottom, so the sheet touches the tooling at three points: the punch tip and the two die shoulders. The bend angle is set by how deep the punch goes, which means one set of tools can produce many angles. Because the sheet isn't fully pressed into the die, it springs back, and the operator has to compensate.
Bottoming
In bottoming, the punch presses the sheet down onto the die so it takes the die's angle. It needs more force than air bending, but gives more consistent angles and less springback.
Coining
Coining uses much higher force to press the sheet into the die, forcing the bend tighter than its natural radius. It's precise, with almost no springback, but it's hard on tooling and needs a lot of tonnage. It's much less common in general job shop work.
Hems and safety folds
A hem folds the edge of the sheet back on itself to give a safe, stiff edge. A safety fold (or open hem) leaves a small gap. Both are usually done in two stages: a sharp bend with an acute tool, then a flattening step.
Key terms in sheet metal bending
What affects bend quality?
Material and grain direction
Different materials bend very differently. Mild steel is forgiving. Stainless springs back more. Harder aluminium alloys and tempers, such as 5083, can crack if the bend runs the wrong way relative to the grain.
The grain that matters is the crystalline grain from rolling, not the surface finish, which catches people out. Grain direction has to be considered when the part is placed on the sheet for cutting, not when it reaches the press brake. By then it's too late. Designers are often unaware of it, so the shop needs to catch it at the quoting or nesting stage.
Thickness, bend length and tonnage
The force needed to bend a part rises with thickness and bend length. A press that handles a 1 m bend in 6 mm steel may not have the tonnage for the same bend at 3 m. Quoting a part your press can't form is one of the most common mistakes in bending.
Bend radius and tooling
The die opening and punch radius set the inside radius. Tighter radii need more force and are more likely to crack. Designs that use several different radii on one part need more tool changes.
Reach and clearance
Some parts can't be bent because of the tooling, not the force. The press needs enough throat depth to reach the bend. And as a part is bent up, already-formed flanges can collide with the punch or the machine. Deep boxes and return flanges often need special tooling, such as gooseneck punches.
Part design
Holes too close to a bend line distort. Flanges that are too short can drop into the die. Symmetrical parts are easier for operators to get the right way round. Our tips for folding and bending laser cut parts cover the main design rules.
The flat pattern
If the K-factor or bend deduction is wrong, the flat blank is cut to the wrong size and the finished part comes out short or long. That's a common problem when the flat pattern produced at quoting is reused for production. For anything other than mild steel, check the unfold uses the right values for that material and thickness. For a cover on a ute, a millimetre won't matter. For a precision part, it will.
Why bending matters when quoting sheet metal parts
Quoting a bent part means answering two questions. What will it cost? And can we actually make it?
What it costs: setup plus handling
The price of bending splits into setup time and bending time.
Setup starts with getting the right punches and dies from the rack. Then it often means setting up several stations along the press. On a 3 m press brake, a part may need three or four setups to complete. Take a 500 x 300 mm tray with flanges on all four sides. The 500 mm sides need a 500 mm tool, but once they're bent, a 500 mm tool would crush them when you turn the part round for the 300 mm sides. So you need a 500 mm station and a 300 mm station. Parts with folds inside other folds can need more.
Some setups add further steps. A bend at an angle to the edge of the part needs a guide on the bed so the part can be positioned correctly. A split fold (where the two ends are bent but the middle isn't) needs an extra stop to locate the part sideways.
Bending time is mostly handling, not pressing. One customer told us a story about a part they quoted with Tempus Tools that was almost 3 m long in 1.6 mm brushed stainless. "It's like trying to fold a piece of tissue paper," was how it was described. It couldn't be scratched, so it couldn't be dragged across tables. It needed three people to lift, a protective film on the tooling, and a full flip part-way through because some bends went the other way. That flip was the most expensive move in the whole job.
Large parts also slow things down at the backgauge. With three or four stops across a long part, you often need a second person to check it's hard up against every stop before the operator presses the pedal.
Can you make it?
The harder question is feasibility. Before quoting a formed part, a shop needs to know:
- Does the press have enough tonnage for this thickness and bend length, without damaging the tooling?
- Does it have the reach (throat depth) and tooling to get to each bend?
- Can each bend be reached without the part hitting the tooling, given the design?
- Are there manufacturability issues, like holes too close to bends?
Without a simulation, many shops add up the bends, allow 10% extra and hope. The risk is quoting a part that can't be folded at all.
In smaller shops, the usual answer is to walk out and ask the press brake operator. That interrupts production. If the operator has to simulate the part on the press controller, that can cost 30 minutes of machine time for one quote. Experienced operators can often look at a drawing and tell you it won't work, but that's not a reliable basis for quoting either. (We've written before about keeping your press brake operator out of quoting.)
Shops with offline press brake programming software can run a simulation on complex parts before they quote. That confirms the part can be bent and gives realistic bend times to price from.
Common quoting mistakes with bent parts
- Pricing only the cutting and treating a formed part like a flat one
- Assuming one setup covers every bend
- Forgetting the handling time for large, thin or cosmetic parts, including extra people, flips and protective film
- Quoting a bend length and thickness the press doesn't have the tonnage for
- Missing collisions and reach problems that make the part impossible to form
- Leaving out other secondary processes on the same part, like welding, countersinking or powder coating
- Pulling the press brake operator off the machine to estimate every job
How shops can price bending more consistently
Most of the cost of bending is predictable if you have rules for it. Part size, weight and the number of bends drive setup and handling time, and those can be priced the same way every time instead of from memory.
A practical example is a handling allowance based on area: once a part exceeds a set size, say 4 square metres, the rule adds time for a second or third person. Heavier parts, cosmetic finishes that can't be scratched, and parts needing a flip can carry similar allowances.
Tempus Tools lets shops set up secondary process pricing for folding, welding, powder coating and other steps, priced from each part's properties, so bending lands on the same quote as the cutting instead of being added by hand. For customers who send 3D models, the 3D sheet metal extractor unfolds STEP and IGES files into flat parts ready to quote. See how it fits together for sheet metal shops.
Rules won't answer the feasibility question on complex parts. That still needs an experienced eye or a simulation. But they take the guesswork out of routine bent parts, and they stop the estimator walking out to the press brake for every quote.
Sheet metal bending and the production handoff
Once a quote is accepted, the information that went into it needs to reach the floor. For bent parts, that means:
- The correct flat pattern for cutting, unfolded with the right K-factor for the material
- The part's orientation on the sheet if grain direction matters
- Bend directions, sequence and any notes on special tooling or handling
- Part labels so operators can match cut blanks to the right job
- Work orders that show which parts need folding and which go straight to dispatch
When that information is missing, the operator works it out again from the drawing, which repeats work done at quoting and invites mistakes. Production documents generated from the quote carry the job details through, so the floor works from the same information the price was based on.
Price the whole formed part
Sheet metal bending is one of the most valuable services a job shop can offer, and one of the easiest to underprice. The press stroke is quick. Setup, tooling, handling and the question of whether the part can be bent at all are where the time and risk sit.
Quote formed parts on the full workflow: cutting, setup, handling and every other process the part needs. Use rules for the routine work, and save the operator's time and the simulation for the parts that need it.
Frequently asked questions
What is sheet metal bending?
Sheet metal bending is the process of forming flat sheet along a straight line into an angle, using force from a press brake or folding machine. Several bends turn a flat blank into brackets, channels, trays and enclosures.
What machine is used for sheet metal bending?
Most shops use a press brake, which forms the sheet between a top punch and a bottom die. Folding machines and panel benders are also common, particularly for long, thin sheet. The machine's tonnage, bed length and throat depth decide which parts it can bend.
What is bend radius in sheet metal?
Bend radius is the radius of the curve formed at a bend, usually measured on the inside. In air bending it's set mostly by the die opening. As a starting rule, keep the inside radius at least equal to the material thickness to avoid cracking.
What is bend allowance?
Bend allowance is the length of material that goes into a bend, measured along the neutral axis. It's added to the flange lengths to calculate the flat blank size, and it depends on the material, thickness, bend radius and K-factor.
Why does bending affect the price of a sheet metal part?
Bending adds setup, tooling changes, operator time and handling, and large or cosmetic parts may need extra people. The press stroke itself is quick, so the cost depends on how many setups the part needs and how hard it is to handle.
How do fabrication shops quote bent parts?
Good quotes check feasibility first (tonnage, reach and tooling), then price setup and handling alongside the cutting. Many shops use pricing rules based on part size, weight and bend count, and run complex parts through bending simulation software before committing to a price.
See how Tempus Tools helps fabrication shops price cutting, bending and secondary processes together, or book a demo.
See how Tempus Tools helps fabricators quote faster and smarter.
Share this post
Articles
Resources
Related Posts
Product updates
0
min read
New integration: Tempus Tools + ECI M1 – from quote to order to ERP, seamlessly
At Tempus Tools, we know that speed and accuracy are everything in a laser cutting job shop, and today we’re announcing a new integration that makes both even easier.
We’re now fully integrated with ECI Software’s M1 ERP system.
What does that mean for your job shop?
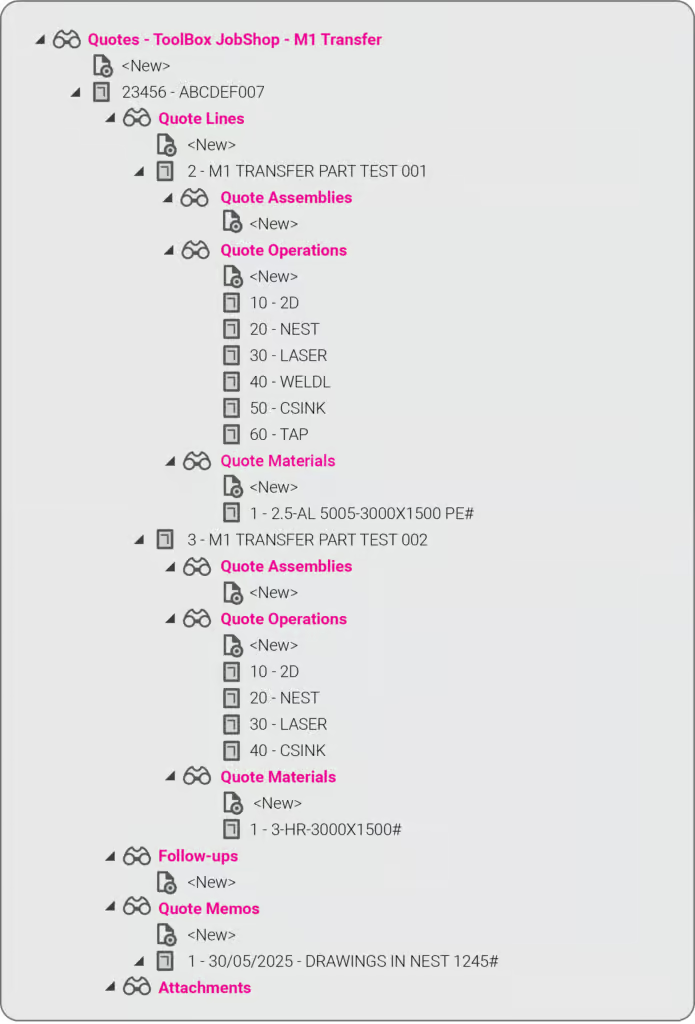
It means you can now send quotes, order details, and production-ready drawings directly from Tempus Tools into your M1 ERP — no more double handling, no more data entry errors, no more jumping between systems.
This integration eliminates any “dead zone” between quoting and production. You get the specialist laser quoting power of Tempus Tools (like lightning-fast nesting, material cost accuracy, and margin control) combined with the operational backbone of M1.
It’s quoting that talks to your shop floor.
We’ve talked about how integrations like Google Drive can supercharge job shop workflows, and this M1 integration is another great example.
Want to learn more or set it up? If you want to avoid the limitations in the generic quoting functions in ERP/MRP software, but still use the rich planning and production features in ERP/MRP software, then get in touch today.
Book a demo or email us at support@tempustools.com and we’ll help you get connected.
Tempus Tools + M1 = quoting to production, finally in sync.
Read blog
Product updates
0
min read
Tempus Tools’ Google Drive integration: 6 ways to supercharge your job shop efficiency
Tempus Tools’ new Google Drive integration automatically saves your quote data and part files to Drive, opening the door to faster, smarter workflows. In this post, we highlight six clever ways job shops are already using it to boost efficiency.
Last month Tempus Tools released a powerful new feature: seamless integration with Google Drive.
Since then, we’ve heard from lots of customers about the innovative ways they have implemented this integration in their job shops, and we wanted to share the best six with you to inspire you to use the feature in your shop.
First, a quick recap: with the Google Drive integration, all your quote data (in CSV format) and production-ready part files can be automatically saved to your chosen Google Drive folder. From here, they can be exported to any number of programs or that data can be manipulated for many use cases, opening up a world of automation, reporting and connectivity for your job shop. We’ve also put together a quick video to show the integration in action.
1. Automate quote data collection for reporting
With every quote automatically saved, you can easily compile and analyse your quote performance over time. Use Google Sheets or your favourite analytics tool to track:
- win/loss rates
- performance across material types
- average order size
- breakdown of secondary processes contributions
This data-driven approach helps you identify trends, optimise pricing and improve customer response times.
2. Connect with ERP/MRP and other business systems
Some apps have native integration with Google Drive, which makes taking in quote data and parts easy, but many need a formal API. Luckily, Google Drive comes with its own API.
Some users have used the Google Drive API to build automations that push quote data directly into ERP, MRP or order management systems. This can streamline order processing, reduce manual data entry and ensure your production schedule is always up to date.
3. Organise your orders by material type
Use the exported quote data to create a parts planner that groups jobs by common material type. This enables you to:
- batch similar jobs for more efficient material usage
- reduce changeover times on machines
- optimise purchasing and inventory management
A simple Google Sheets script or integration with a dashboard tool can make this process nearly automatic.
4. Integrate with project management tools
Connect your quote data with popular tools like ClickUp, Monday.com or Airtable. Build custom dashboards and planners for your factory, visualise job statuses and assign tasks to your team-all based on real-time quoting data. These tools don’t require coding or a developer and anyone can work wonders. These types of projects boost collaboration on the shop floor and keep everyone aligned on priorities.
5. Create a scheduling calendar from time calculations
Use the time estimates in your quote data to automatically populate a production calendar. With a Google Calendar integration, you can:
- visualise machine and operator workloads
- identify bottlenecks before they happen
- easily adjust schedules as new jobs come in
This proactive scheduling helps you deliver on time, every time.
6. Enable automated notifications and workflows
Set up Google Drive triggers (using tools like Zapier or Google Apps Script) to notify your team when new quotes are confirmed as orders, or to kick off downstream processes-like updating CRM records or ordering materials.
Getting started is easy
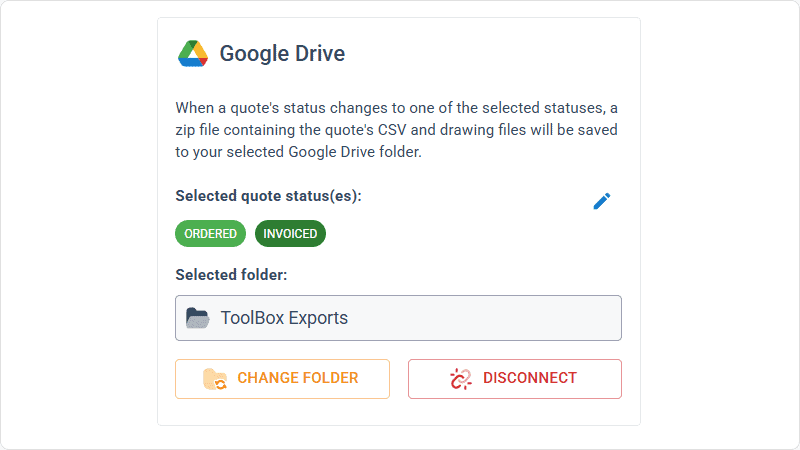
- Go to Settings > Organisation settings > Integrations in your Tempus Tools Tempus Tools account
- Connect your Google Drive and select your preferred folder
- Choose the quote statuses that will trigger automatic file saving
- Start building automations and workflows that fit your shop’s needs
This integration is designed to be flexible-whether you want to automate reporting, connect with business systems, or simply keep your files organised, Tempus Tools and Google Drive make it possible.
Ready to enhance your job shop efficiency? Try the new Google Drive integration today.
Read blog
Articles
0
min read
Is expensive, non-dedicated software holding you back from effortless laser cutting quoting?
Many laser cutting job shops still rely on generic or overly complex software, slowing down RFQ response times and creating bottlenecks that hurt profitability. Tempus Tools offers a fast, intuitive, and purpose-built quoting solution—with powerful features, simple setup, and transparent pricing—to help shops quote accurately, streamline production, and stay competitive.
Laser cutting is a precise task, requiring machinery tailored to specific requirements. Profitability is significantly boosted by the ability to be able to respond quickly to customer requests for quotes (RFQs), and efficiently deliver the product.
“With the time and energy often spent on selecting the right laser cutting machine, it’s amazing how often software is overlooked as a driver of productivity,” says Tempus Tools Head of Global Sales, Mark Washington.
“Sometimes laser cutting companies are stuck using software that wasn’t specifically designed for job shops, but it’s all that their team is used to using. Other times, expensive software is implemented, but only a small fraction of the features are actually used,” he says.
“And in many cases, it becomes so complex that a specialist is hired to manage quoting via the software – but what happens if they leave the company?”
Tempus Tools is the creator of dedicated quoting software, Tempus Tools, which can provide fast, accurate, and consistent laser cutting quotes that are professionally presented, ready to send back to the customer.
“Using software that isn’t specifically designed for laser cutting is like using a cricket bat to play tennis. It might get the job done, but it would be far more efficient and accurate with the tools designed for the job!” says Mark (pictured, right).
“In addition to providing quotes in minutes, Tempus Tools can also produce production documents with the click of a button, to add further efficiency to running a job shop floor,” he adds.
A shift in the industry
With customers demanding faster service, the industry is shifting to tailored laser cutting quoting solutions, to enhance their RFQ response times, and Mark sees this as part of a larger global trend.
“It’s evident across a number of industries – smarter players want to utilise technologies specifically targeted to their industry to out-pace competitors. And laser cutting job shops are enthusiastically getting on board with this trend,” he says.
“Tempus Tools has been specifically designed for laser cutting job shops. It’s quick to set up, intuitive, and user-friendly, so the entire team can use it with minimal training, instead of relying on one specialist.”
Tempus Tools cloud-based laser cutting quoting software can be set up with information on material price, cutting time, labour, and other relevant information, to generate quotes quickly and accurately, with repeatability.
“The Tempus Tools team has decades of experience in the laser cutting industry, from the shop floor, through to management, and running their own laser cutting enterprises, so we know the industry inside out – and we can support through setup and every step of the journey, for no additional charges,” adds Mark.
“A major inhibitor of laser cutting quoting software has often been cost, with powerful software that can do it all costing thousands per month. But if you only need dedicated laser cutting quoting software, our plans start from US$100 per month, and are packed full of features you will actually use,” he says.
Switching software – overcoming challenges
Even with the knowledge of the benefits of dedicated laser cutting quoting software, job shops can be hesitant about the time involved in switching, says Mark. He notes some of the main concerns:
- Time – often job shops have tried other software implementations and it’s taken months, and they just cannot afford to spend that time again. But Tempus Tools isn’t like other software. For a job shop with one laser, press brake, and standard secondary processes, set up takes less than 90 minutes.
- Staff training – job shops often believe their staff don’t have the time or capacity to learn a whole new software. But again, Tempus Tools is different. It’s designed to be user-friendly, easy to learn, and staff end up doing their jobs more efficiently, and enjoying the features right away.
- Hidden costs – this is a big factor for any software, and job shops are highly alert to cheap upfront costs, followed by lots of add-ons. No one likes to be “nickel and dimed”. For Tempus Tools, it’s a monthly or yearly subscription, and that’s all. No extra charges for support, upgrades, or training. Features all have a set pricing that’s clear from the outset.
- Too many programs – some job shops have two, three, or more different software programs – why add more, especially if they don’t talk to each other? That’s a totally valid concern. Tempus Tools outputs a CSV as standard with all the quote data, making integration seamless and easy.
“The Tempus Tools leadership team has decades of experience working from the shop floor to the top floor, so they understand the pain of changing software, and have designed Tempus Tools to be effortless and simple,” says Mark.
Tempus Tools features
Tempus Tools features that have been specifically designed for laser cutting job shops include:
- 3D model extractor. Identify, extract and unfold sheet-metal parts directly from 3D assemblies without a 3D software package.
- PDF to CAD convertor. Convert a vector PDF into a CAD file instantly. No tracing, no CAD package, just click on a part and extract it into your quote.
- Tube quoting. Easily drag and drop rectangular, square or round hollow sections into the tube module. It quickly calculates highly accurate cutting time and material consumption for pricing.
- Web Store. Let your customers get instant pricing and place orders from your website 24/7 with an online quoting portal.
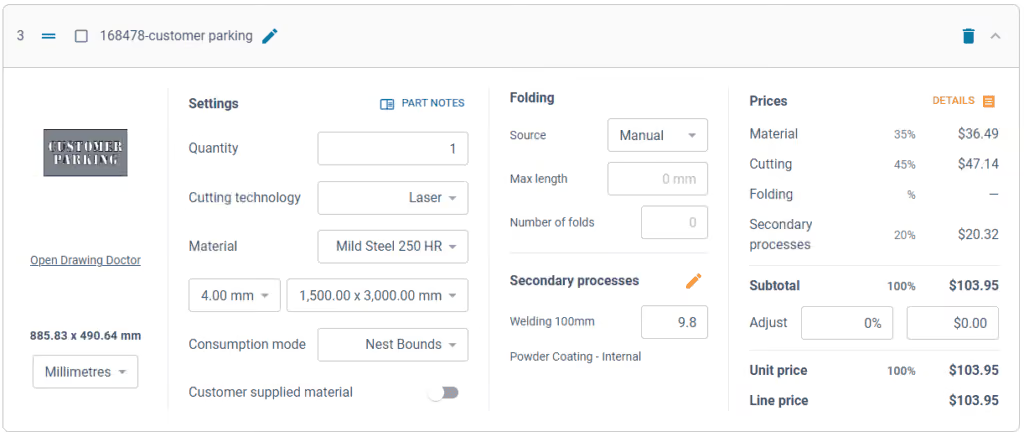
- Secondary processes. Get accurate and consistent folding prices quickly using the built-in folding algorithm developed by specialists with decades of experience using brake presses.
- Drawing Doctor®. Upon upload of a 2D DXF or DWG file, Drawing Doctor® automatically corrects for double lines, dimensions, and small end points that are hidden in some drawings.
- Part Library. Part Library allows you to save parts that you’ve produced for a customer for re-use. Saves time on repeat orders and quotes, by dropping an existing part straight into the quote, ready to calculate, based on the latest pricing.
“These are just a few of our most popular features, but there are lots more within Tempus Tools, and our development team is constantly listening for customer feedback to determine what new features can be added,” says Mark.
“So for effortless laser cutting quoting, don’t let software hold you back, let it be the catalyst that drives business growth. We offer an obligation-free trial of Tempus Tools so that laser cutting job shops can see the difference for themselves.”
Read blog